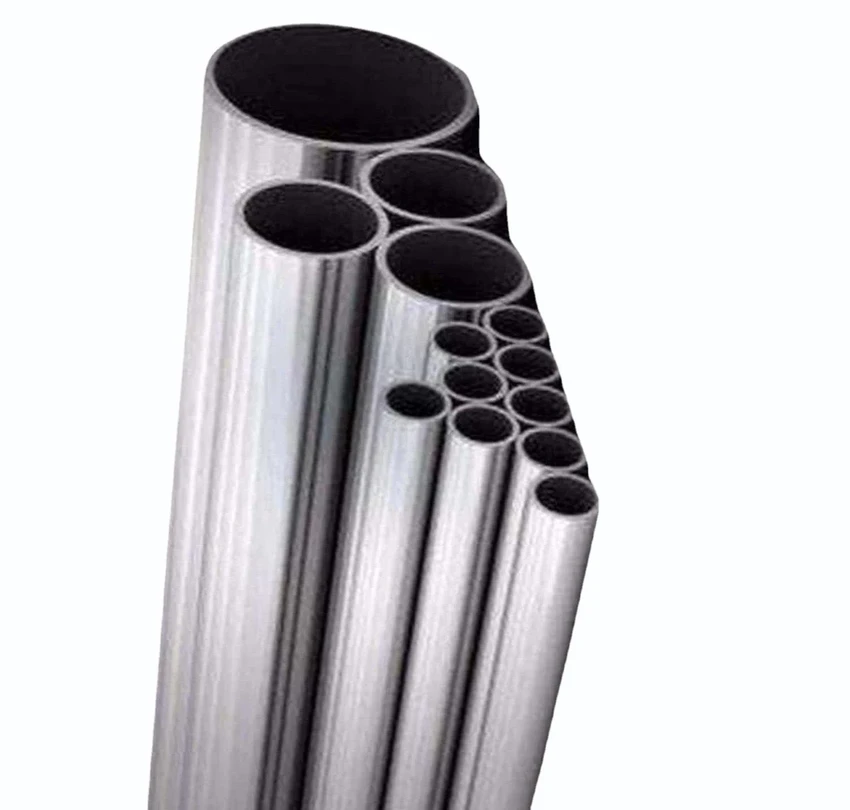
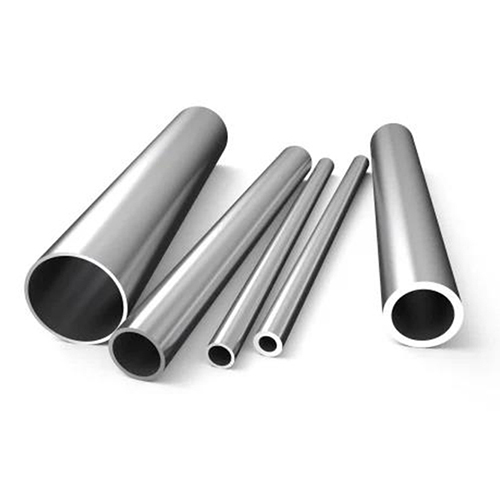
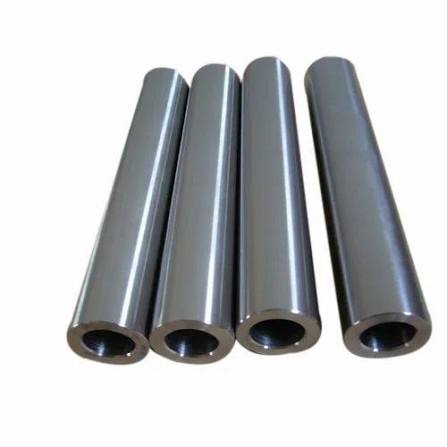
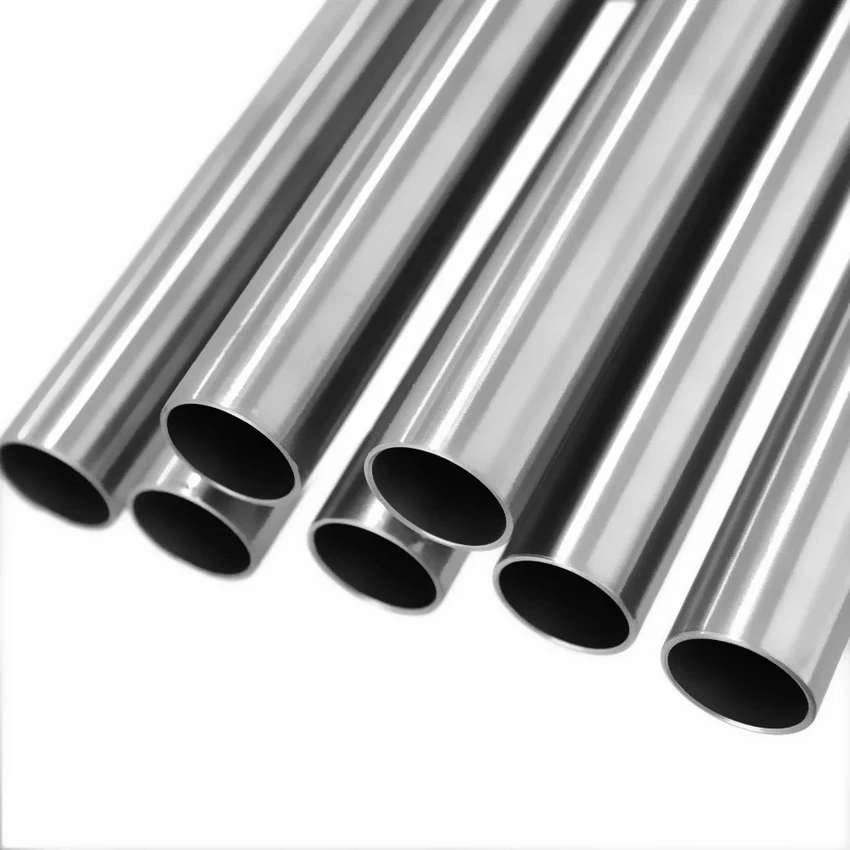
When engineering chemical synthesis reactors, chlorine dioxide bleaching towers, hot brine recycling loops, or hazardous waste neutralization setups, fluid containment pathways face aggressive electrochemical stress. Under continuous exposure to localized acid concentrations, high-temperature halides, and fluctuating pH balances, standard stainless steels and even versatile unalloyed titanium grades can experience localized passive film breakdown. This breakdown leads to devastating crevice corrosion beneath gaskets, tube sheets, or structural scale deposits. Serving as a premier manufacturing entity, we forge, extrude, and precision-machine heavy-duty Titanium Grade 7 Pipes engineered explicitly to maintain a permanent leak-proof containment barrier. Grade 7 titanium (UNS R52400 / W.Nr. 3.7235) represents the ultimate palladium-stabilized micro-alloyed modification of commercially pure titanium, optimized specifically for aggressive processing media.
The primary metallurgical advantage of a Titanium Grade 7 pipe lies in its target addition of 0.12% to 0.25% palladium. While matching the baseline physical parameters, excellent formability, and superb weldability of Grade 2, this intentional palladium inclusion fundamentally alters the alloy's electrochemical behavior. Palladium acts as a powerful cathodic modifier, shifting the corrosion potential of the material in a noble direction. This forces the spontaneous and instantaneous reformation of a highly resilient microscopic titanium dioxide ($TiO_2$) passive layer inside restricted crevices, even when exposed to severe reducing acid media like dilute hydrochloric or sulfuric acids. Forged and cold-pilgered from premium certified billets, our seamless pipes completely eliminate internal micro-porosity and wall variations, providing exceptional resistance to localized crevice tracking and stress corrosion cracking.
Our heavy industrial manufacturing facility in Mumbai leverages state-of-the-art technological infrastructure to transform high-purity, traceably certified Titanium Grade 7 billets and plate stock into high-performance industrial pipelines. For our seamless piping inventory, we operate advanced high-tonnage hydraulic piercing and hot-extrusion presses alongside automated cold-pilgering mills. Because titanium and its palladium-stabilized variations exhibit exceptional mechanical toughness and rapid work-hardening traits, the cold-working sequence must be managed within highly precise mechanical and thermal windows to re-align the internal micro-grain flow along the exact longitudinal axis of the pipe body, yielding vastly superior burst pressure thresholds and tight dimensional tolerances compared to standard hot-rolled options.
Following primary forming, all titanium pipes pass through mandatory thermo-mechanical heat treatment regimens conducted within protective, oxygen-free controlled vacuum atmospheres to prevent interstitial oxygen, nitrogen, or hydrogen contamination which causes metal embrittlement. This critical sequence completely relieves internal mechanical stresses, breaks down coarse crystalline formations, and restores maximum material ductility. Our precision finishing lines utilize automated straightening rollers and high-speed CNC machine tools to finish pipe ends, executing precise weld-bevel preparation (typically 37.5° matching ASME B16.25 standards) to enable rapid, high-integrity field fit-up and circumferential butt-welding at the job site.
To satisfy the strict safety mandates of regulated chemical processing networks, hazardous acid utilities, defense operations, and global maritime safety bodies, every single production batch undergoes thorough destructive and non-destructive testing (NDT) protocols. Our internal quality control laboratory features certified technicians who execute 100% Positive Material Identification (PMI) using advanced spectrometers to guarantee precise chemical alloy grade authenticity before any batch proceeds to forming blocks.
Because pipelines operating under full hydrodynamic loads experience maximum structural stress, internal volumetric auditing is an absolute priority. We perform 100% non-destructive **Ultrasonic Testing (UT)** and **Radiographic Verification (RT)** across all high-pressure components to verify the complete absence of sub-surface micro-fissures, gas porosity, or internal forging flaws. All pipes are subjected to mandatory Hydrostatic Pressure Containment testing up to strict code limits, accompanied by digital profile gauges to map wall thickness tolerances and ensure absolute geometric uniformity from end to end.
The operational lifespan, mechanical resilience, and chemical defense of an industrial Titanium Grade 7 pipe depend entirely on its specific chemical composition and its primary structural classification.
The chemical formulation of Grade 7 is precisely regulated to achieve maximum cathodic protection and crevice immunity by controlling the palladium threshold and interstitial traces:
| Alloying Element | Palladium (Pd) | Iron (Fe) | Oxygen (O) | Carbon (C) | Nitrogen (N) | Hydrogen (H) | Titanium (Ti) |
|---|---|---|---|---|---|---|---|
| Specification Range | 0.12–0.25 | 0.30 Max | 0.25 Max | 0.08 Max | 0.03 Max | 0.015 Max | Balance |
Note: Titanium Grade 7 represents the most corrosion-resistant variant of the commercially pure family. The structural inclusion of palladium provides extreme security against localized pitting in low-pH reducing streams where unalloyed Grade 2 and Grade 1 would undergo active dissolution.
Depending on line dimensions, operating pressure class parameters, and budget allocations, we supply industrial piping across two foundational configurations:
| Parameter | Seamless Pipe (ASTM B861) | Welded Pipe (ASTM B862) |
|---|---|---|
| Manufacturing Process | Hot-extruded and cold-pilgered from solid forged titanium-palladium billets. Features an uninterrupted solid cylinder wall structure without welds. | Formed from continuous precision strip or plate, welded longitudinally via automated TIG/Plasma arc lines under strict inert gas shielding. |
| Pressure Capabilities | Maximum hydrostatic retention; completely eliminates the risk of directional seam failure under severe cyclic loads. | Moderate to high pressure; governed by a joint efficiency factor ($E = 0.85$ or $1.00$ based on volumetric NDT status). |
| Size Range Spectrum | Standard availability typically restricted from 1/2" NB up to 12" NB due to heavy hydraulic extrusion limits. | Virtually unrestricted; ideal for large-diameter process lines stretching from 1/2" NB up to 36" NB and above. |
| Wall Thickness Uniformity | Excellent, though slight wall concentricity variations can occur over long structural lengths. | Ultra-precise wall thickness uniformity, as the starting point is a high-accuracy rolled titanium sheet or plate. |
Our production engineering strictly follows global dimensional codes to ensure hassle-free integration with global piping infrastructure, valves, flanges, and fittings.
| Parameter | Specification Details |
|---|---|
| Design Standards | ASME B36.10M (Dimensional alignment for general pipe sizes), ASME B36.19M (Standard dimensional codes for titanium and stainless pipe schedules), DIN, ISO, EN codes |
| Material Specifications | ASTM B861 (Titanium and Titanium Alloy Seamless Pipe), ASTM B862 (Titanium and Titanium Alloy Welded Pipe), DIN 17861, EN 10216-5 |
| Common Material Grades | Palladium-Stabilized Commercially Pure Grade 7 Titanium (UNS R52400 / W.Nr. 3.7235) |
| Wall Thickness Schedules | Sch 5S, Sch 10S, Sch 40S (Standard Wall / STD), Sch 80S (Extra Heavy / XS) |
| Facing End Layouts | Beveled Ends (BE standard for butt-welding), Plain Ends (PE for socket-welding or slip-on layouts), Threaded Ends (TE matching NPT criteria) |
| Size Specification Matrix | 1/2” NB up to 36” NB standard coverage (Custom wall dimensions and large-diameter pipelines executed to blueprint criteria) |
| Testing Regimens | 100% PMI verification, Hydrostatic Leak Containment, Volumetric Ultrasonic/Radiographic Seam Check, Hardness check, Flattening and Bend tests |
For global engineering, procurement, and construction (EPC) firms, plant turnaround contractors, and infrastructure developers handling high-volume volatile networks, sourcing traceably certified industrial titanium pipelines is a precise task. Partnering with a dedicated distribution channel in Mumbai gives you a distinct operational edge.
We provide volume-based commercial discounts, comprehensive material traceability certifications (MTC EN 10204 3.1/3.2), and durable, sea-worthy bundling packaging designed to prevent transit surface scratches, end bevel distortion, or bending. Pipes are protected with protective end plastic caps and wrapped securely, ensuring your high-value components arrive at the project site ready for immediate welding and installation.
Our focus on precision dimensional control and zero-defect quality validation has earned strong international trust. Operating from the export hub of Mumbai, we regularly ship high-reliability seamless and welded titanium pipes to offshore oil exploration platforms in the Middle East, specialized chemical and marine infrastructure operations in Europe, and water desalination complexes across Southeast Asia.
Every export order passes through a strict final quality checkpoint, including full dimensional analysis, 100% PMI validation, and hydrostatic proofing checks. We package shipments in heavy-duty, seaworthy bundles or wooden crates equipped with moisture-resistant barriers and protective end protectors. This ensures your high-yield components arrive at the project site ready for immediate installation.
| Titanium Grade 7 Piping – Technical Specifications | Details |
|---|---|
| Size Specification Range | 1/2" to 36" (Complete Nominal Bore Spectrum for lightweight, high-crevice fluid containment) |
| Wall Thickness Range | Sch 5S up to Sch 80S (Complete coverage from thin-wall utility to extra-heavy structural wall schedules) |
| Type Configurations | Seamless Hot-Extruded & Cold-Pilgered Pipe, Longitudinally Welded (TIG/Plasma) Pipe Spectrum |
| End Finish Formats | Weld Beveled Ends (37.5° Bevel Angle), Square Cut Plain Ends, Male Threaded Ends (NPT) |
| Surface Protection Options | Cleaned Acid-Pickled Surface, Bright Vacuum Annealed Finish, Protective Wrapping with End Cap Enclosure |
| Testing Protocols | Hydrostatic Proof Testing, Radiographic/Ultrasonic Seam Audit, PMI analysis, Flattening & Bend tests, Hardness verification |
| Certification Scope | EN 10204 3.1 / 3.2 Mill Test Certification, Compliance with NACE MR0175 / Sour Service environments |
Find the Best Quality Industrial Solutions and Workspace Furniture at Factory Prices.