Inconel 600 Flanges Supplier in Mumbai
The Metallurgy and Surface Finish Seating Face Engineering
The operational lifespan and environmental resilience of an Inconel 600 flange depend entirely on its specific chemical composition and the precision finish of its mating connection profile.
Chemical Composition Matrix (UNS N06600) (%)
The chemical formulation of Inconel 600 is precisely regulated to deliver robust physical tensile properties from cryogenic limits up to an elevated service threshold of 1095°C:
| Nickel (Ni) |
Chromium (Cr) |
Iron (Fe) |
Manganese (Mn) |
Silicon (Si) |
Copper (Cu) |
Carbon (C) |
| 72.00 Min |
14.00–17.00 |
6.00–10.00 |
1.00 Max |
0.50 Max |
0.50 Max |
0.15 Max |
Precision Sealing Face Profiles and Roughness Height Management
Equally critical is the dimensional machining of the sealing face. When tightening a superalloy connection, the mating surfaces must compress the gasket with absolute uniformity to contain high-energy fluids. Our specialized CNC turning centers machine precise concentric or phonographic serrations into the Raised Face (RF) profiles, maintaining a strict 125–250 micro-inch AARH (Arithmetic Average Roughness Height) surface finish. This targeted roughness forces the gasket material to cold-flow directly into the micro-grooves, creating an impenetrable, leak-proof barrier capable of containing Class 150# to Class 2500# process streams. For high-pressure operations, high-precision Ring Type Joint (RTJ) grooves are machined to accept metallic ring gaskets.
Primary Inconel 600 Flange Joint Configurations
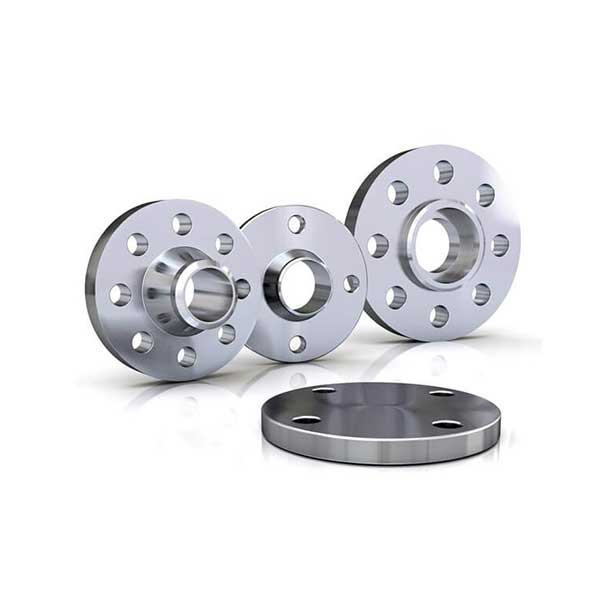
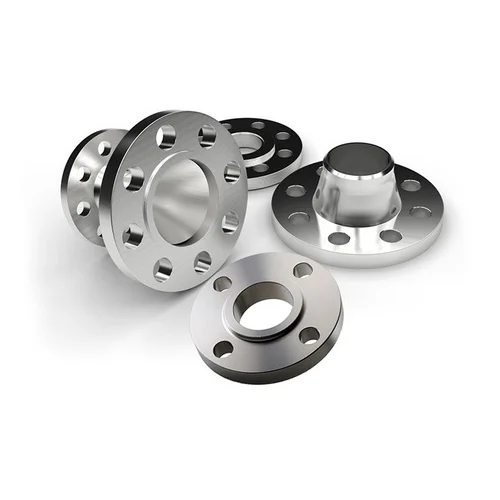
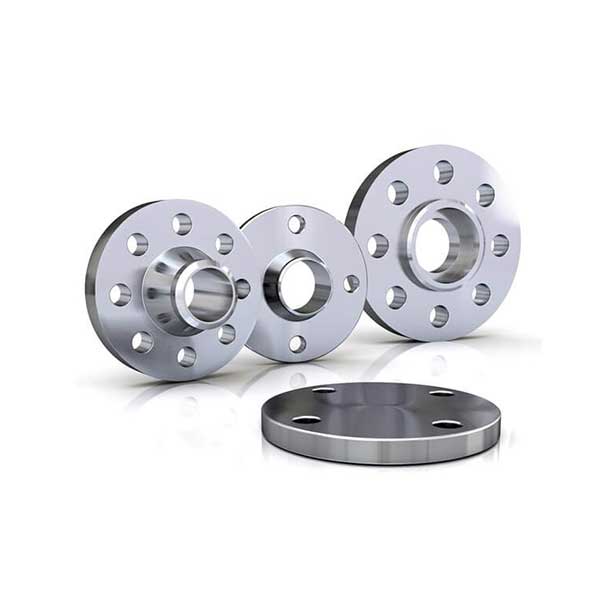
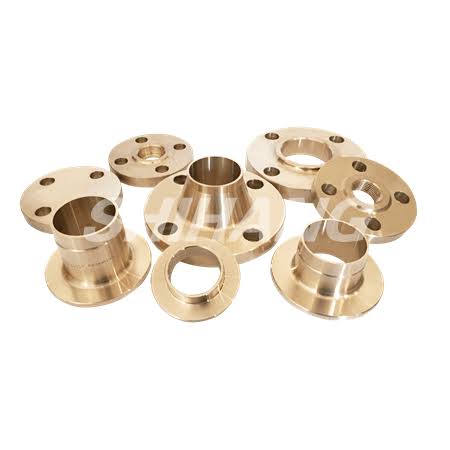
Depending on line fluid velocities, internal pressure drops, and general pipeline routing parameters, we manufacture a comprehensive suite of body designs:
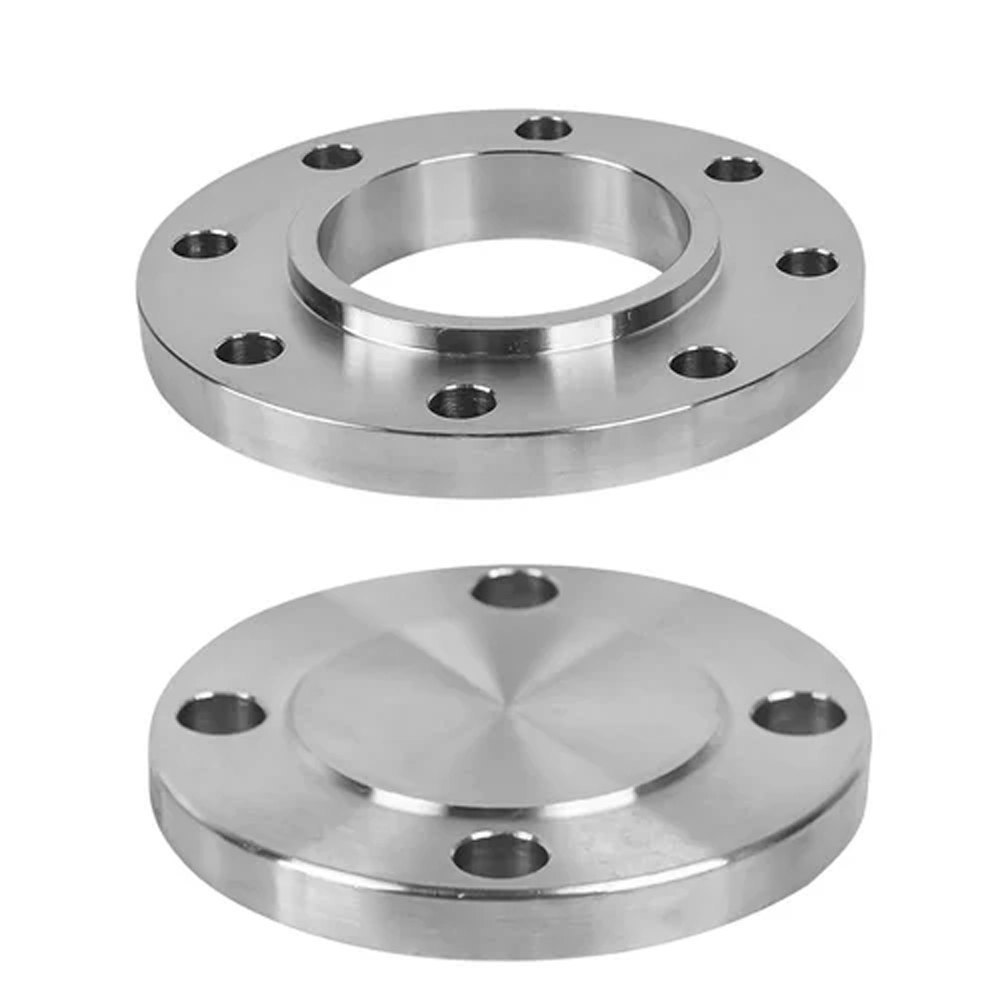
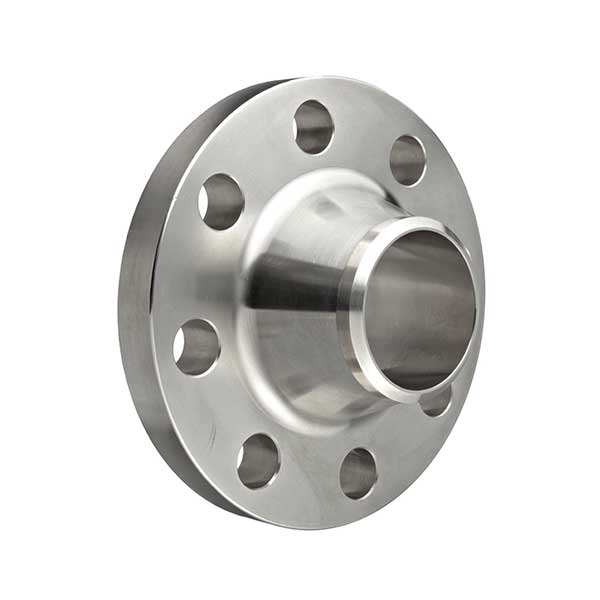
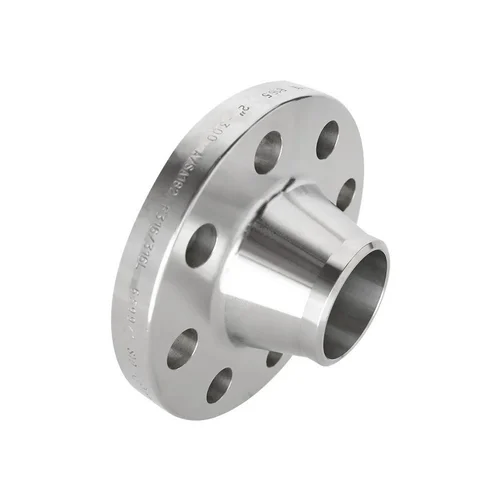
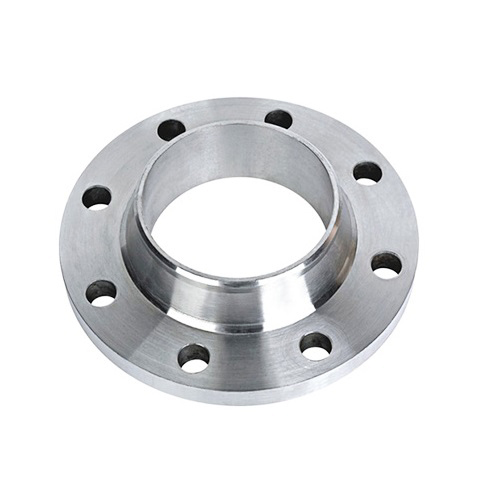
- Weld Neck Flanges (WNRF): Engineered with a long, tapered structural hub that mirrors the pipe's internal wall thickness. This transfers mechanical stress directly into the line, making it ideal for high-pressure, high-vibration, or extreme thermal expansion zones.
- Slip-On Flanges (SORF): Features an internal bore slightly larger than the outside diameter of the pipe. It slides smoothly over the line and is secured with dual internal and external structural fillet welds, making it a highly cost-effective and easy-to-align option for processing manifolds.
- Blind Flanges (BLRF): A solid forged disc with no center bore used to permanently seal specialized inspection openings or terminate a pipeline run under full hydrodynamic loads.
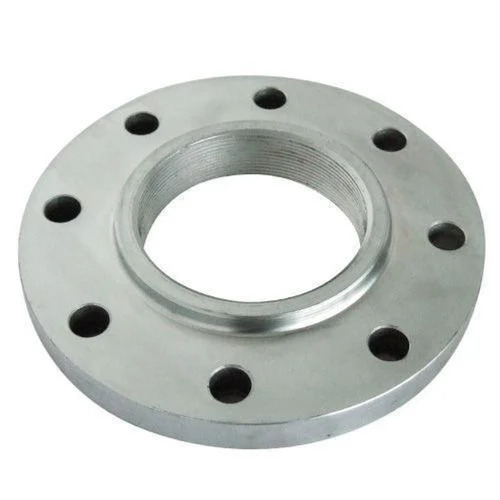
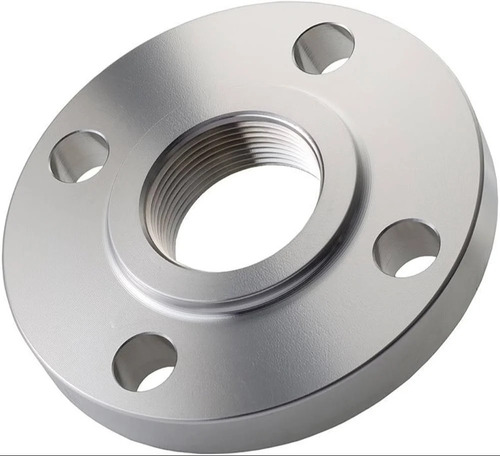
- Socket Weld & Threaded: Ideal for small-bore chemical dosing networks where internal space limits welding options or where field welding poses localized safety risks.
Dimensional and Material Specifications
Our production engineering strictly follows global dimensional codes to ensure hassle-free integration with global piping infrastructure and commercial industrial systems.
| Parameter |
Specification Details |
| Design Standards |
ASME B16.5 (1/2" to 24"), ASME B16.47 (Series A & B large diameter boundaries up to 60"), DIN, EN 1092-1 Type 11/12/05 |
| Material Specifications |
ASTM B564 (Standard specification for Nickel Alloy Forgings), ASME SB564 standards |
| Common Trade Names |
Inconel 600, Alloy 600, UNS N06600, W.Nr. 2.4816, Ferrochronin 600 |
| Pressure Classes |
Class 150, 300, 400, 600, 900, 1500, 2500 LBS / Metric PN6 to PN400 parameters |
| Facing Design Formats |
Raised Face (RF Serrated), Flat Face (FF), Ring Type Joint (RTJ oval/octagonal groove ring) |
| Size Range Spectrum |
1/2” NB up to 24” NB standard (Large large-diameter custom dimensions manufactured to order) |
| Testing Regimens |
100% PMI analysis, Volumetric Ultrasonic Hub Check, CMM Geometric Audit, LPT, Hardness check |
Driving B2B Procurement via an Authorized Flanges Dealer in Mumbai
For global engineering, procurement, and construction (EPC) firms, original equipment manufacturers (OEMs), and nuclear/thermal facility builders handling intense high-temperature environments, sourcing traceably machined joints is crucial. Partnering with a dedicated distribution channel in Mumbai gives you a distinct operational edge.
We provide volume-based commercial discounts, comprehensive material traceability certifications (MTC EN 10204 3.1/3.2), and durable, sea-worthy packaging designed to prevent edge dents, thread cross-threading, or seating face scratches during transport. Additionally, our sales engineers provide direct technical support to procurement teams, verifying imperial bolt patterns, matching pipe schedules, and wall-thickness compatibility to match project parameters perfectly.
Inconel 600 Flanges Exporter in Mumbai
Fulfilling Global Contracts as a Top Superalloy Flanges Exporter from Mumbai
Our focus on precision machining and zero-defect forging has earned strong international trust. Operating from the export hub of Mumbai, we regularly ship high-reliability Inconel 600 flanges to high-temperature furnace manufacturing networks in Europe, specialized chemical complexes in the Middle East, and nuclear engineering setups across Southeast Asia.
Every export order passes through a strict final quality checkpoint, including full dimensional analysis, 100% PMI validation, and face flatness checks. We package shipments in heavy-duty, export-grade wooden cases equipped with moisture-resistant barriers and tailored face protectors. This ensures your components arrive at the project site ready for immediate installation.
Technical Specifications Summary
| Inconel 600 Flanges – Technical Specifications |
Details |
| Size Range Spectrum |
1/2" to 24" under standard ASME metrics (Custom large diameters up to 48" available) |
| Pressure Designation |
150#, 300#, 400#, 600#, 900#, 1500#, 2500# LBS, metric PN 6 to PN 400 Bar ratings |
| Type Configurations |
Weld Neck (WNRF), Slip-On (SORF), Blind (BLRF), Socket Weld (SWRF), Lap Joint (LJF), Threaded |
| Face Design Options |
Raised Face (Serrated RF), Flat Face (FF), Ring Type Joint (RTJ Groove), Tongue & Groove |
| Manufacturing Process |
100% Forged / Vacuum Annealed & Precision CNC Bored & Machined Finished |
| Testing Protocols |
Hydrostatic Pressure Containment, PMI validation, Hardness check, Volumetric Ultrasonic Check, LPT |
| Certification Scope |
EN 10204 3.1 / 3.2 Mill Test Certificate, Compliance with NACE MR0175 / ISO 15156 Sour Service |