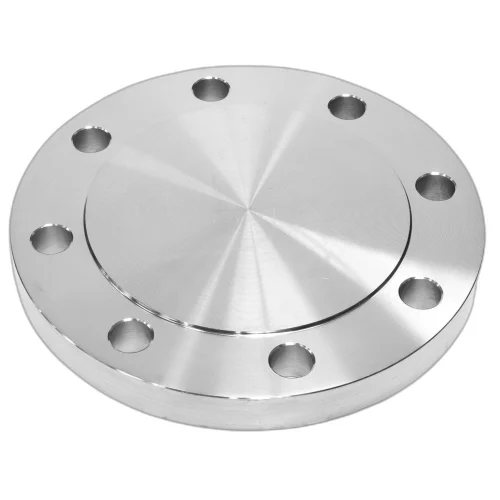
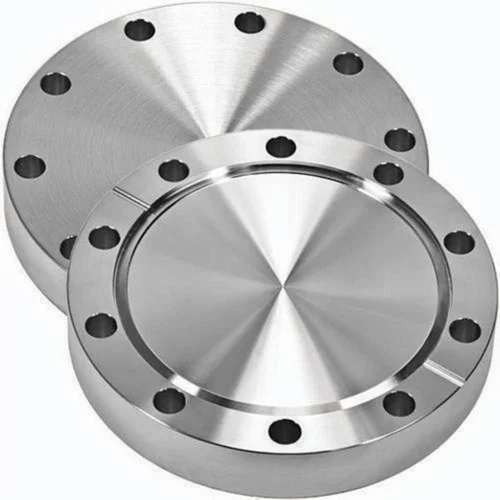
Carbon Steel Blind Flanges Supplier in Mumbai
The Metallurgy and Surface Finish Seating Face Engineering
The operational lifespan and mechanical resilience of a carbon steel blind flange depend entirely on its specific chemical composition and the precision finish of its mating connection profile.
Chemical Composition and Targeted Material Grade Adaptability
Industrial utility loops rely on specific carbon ratios to maintain an optimal balance between mechanical tensile properties and easy field weldability:
- ASTM A105 / A105N (Normalized Forged Carbon Steel): The premier industry baseline standard for pressure systems, delivering excellent structural yield strength, uniform density, and robust mechanical stability in ambient to high-temperature configurations.
- ASTM A350 LF2 Class 1: A specialized low-carbon formulation engineered explicitly to preserve exceptional structural notch toughness and prevent brittle fractures in low-temperature utility loops down to -46°C.
- ASTM A694 (Grades F42 to F70): High-yield carbon steel forgings engineered specifically for high-pressure transmission pipelines in oil and gas gathering systems, matching advanced pipeline strength requirements.
Precision Sealing Face Profiles and Roughness Height Management
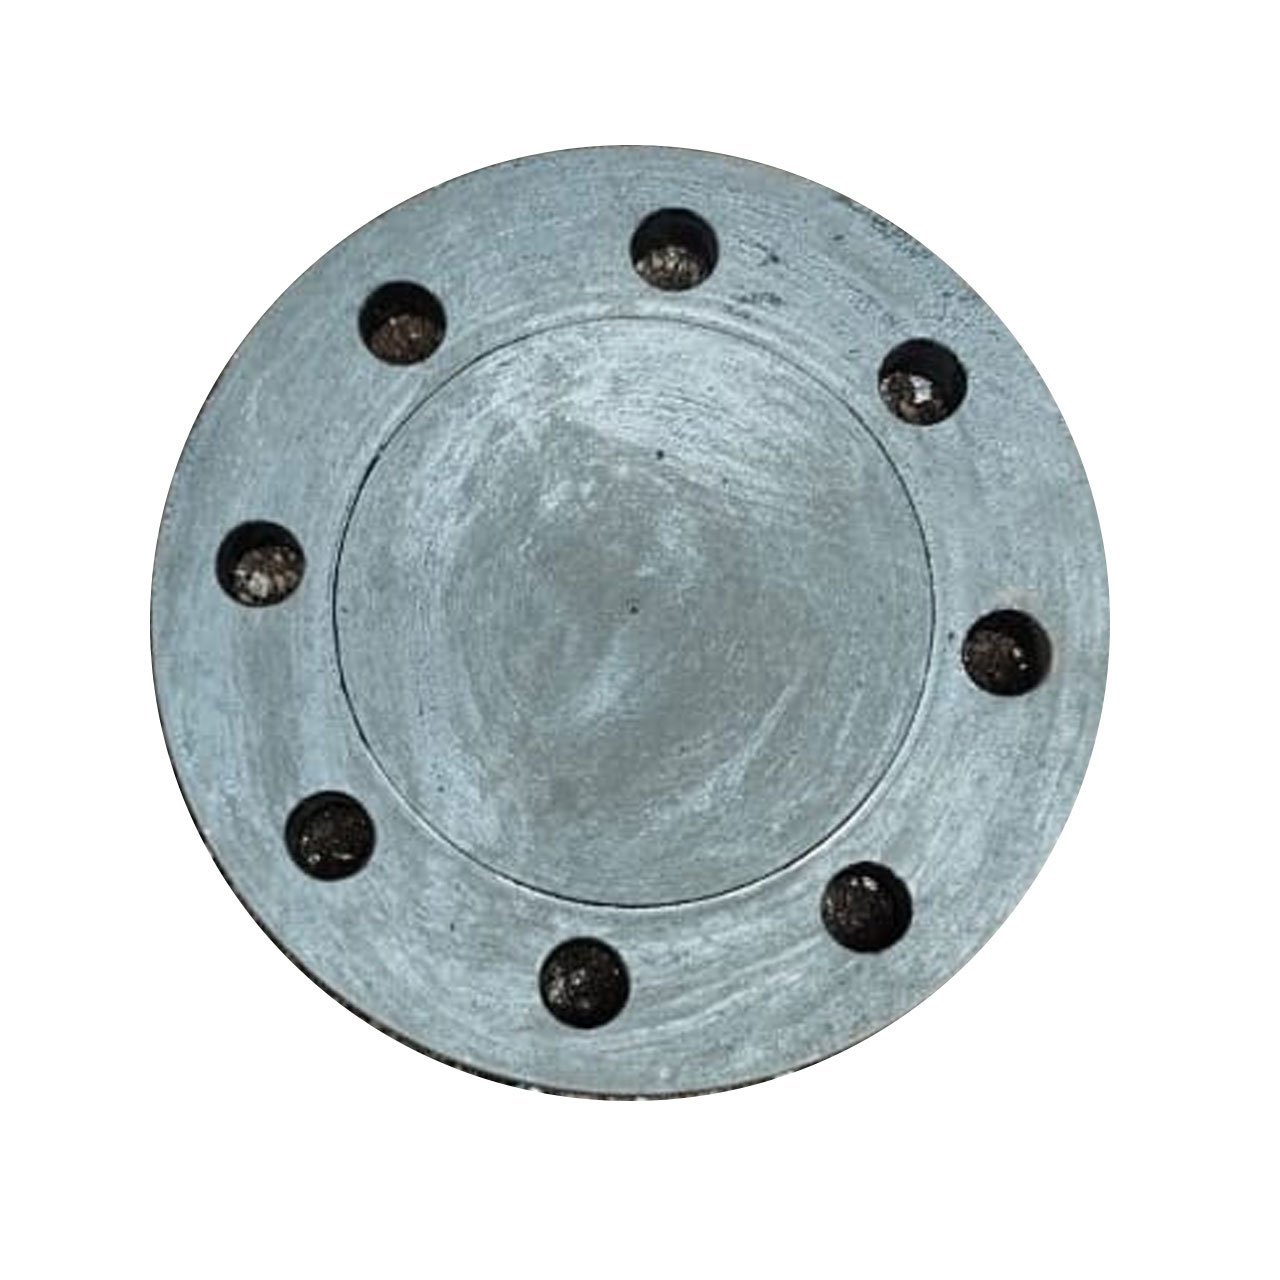
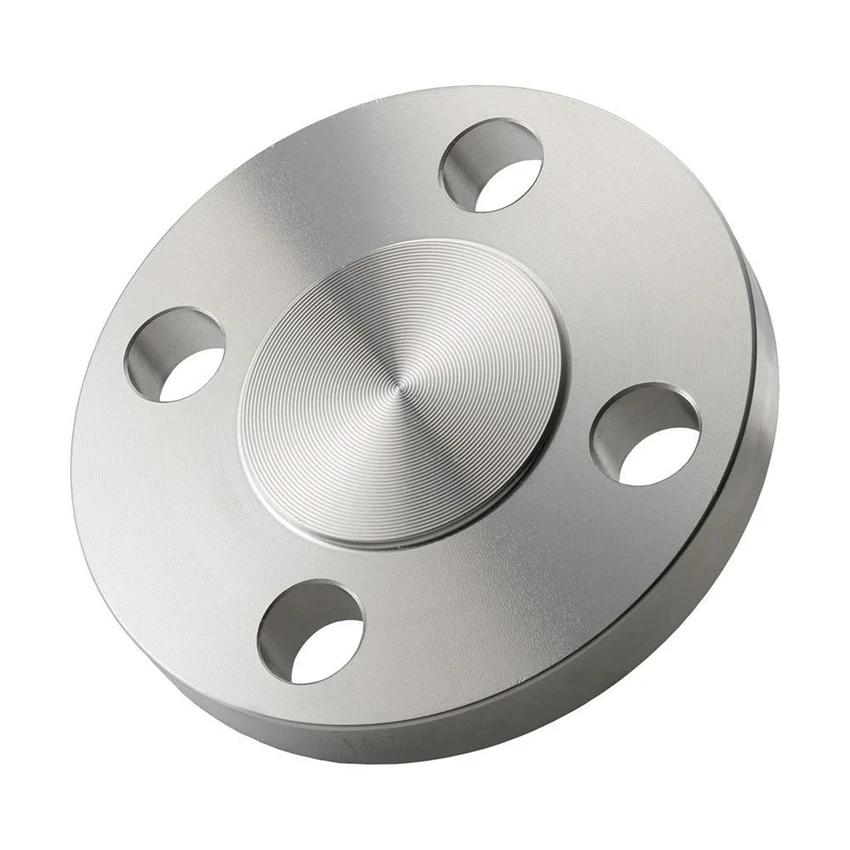
Equally critical is the dimensional machining of the sealing face. When tightening a blind connection, the solid mating surface must compress the gasket with absolute uniformity against the companion flange to contain high-energy fluids. Our specialized CNC turning centers machine precise concentric or phonographic serrations into the Raised Face (RF) or Flat Face (FF) profiles, maintaining a strict 125–250 micro-inch AARH (Arithmetic Average Roughness Height) surface finish. This targeted roughness forces the gasket material to cold-flow directly into the micro-grooves, creating an impenetrable, leak-proof barrier capable of containing Class 150# to Class 2500# process streams. For high-pressure operations, high-precision Ring Type Joint (RTJ) grooves are machined to accept metallic ring gaskets.
Primary Carbon Steel Blind Flange Specialized Layout Variations
Depending on the pipeline geometry, line size, and maintenance preferences, we supply solid closing components across several distinct variations:
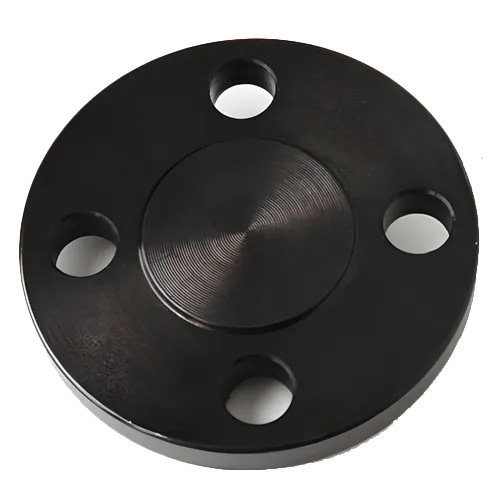
- Standard Raised Face Blind (BLRF): The foundational industrial baseline featuring a raised outer border matching standard pipe dimensions, allowing for quick deployment on standard flanged piping assemblies.
- Tapped Carbon Steel Blind Flanges: Engineering with a small, concentric female-threaded center opening (typically NPT/BSPP) to allow for the attachment of a pressure monitoring instrument, drain valve, or secondary bypass injection point directly through the solid blocking plate.
- Spectacle Blind / Figure-8: A specialized dual-component assembly consisting of a solid blind disk linked to an open flow ring, allowing technicians to physically rotate the unit between active flow and secure shutdown states during routine safety audits.
Primary Coating Configurations and Surface Finishing
Because carbon steel lacks the natural passivation traits of stainless alloys, applying an external barrier coat is essential to prevent atmospheric rust and galvanic oxidation during transit or storage:
- Anti-Rust Oil Coating: A light, temporary layer of technical translucent oil applied immediately after CNC machining to protect faces during inland freight and short-term storage.
- Black Phosphated Finish: An industrial chemical conversion coating that binds a protective layer of black iron-phosphate to the steel body, enhancing wear resistance and basic corrosion defense.
- Hot-Dip Galvanized (ASTM A153): Fusing the forged component inside a molten zinc bath to form a thick, metallurgy-bonded iron-zinc alloy shield, providing maximum rust protection in severe outdoor, underground, or high-humidity marine zones.
Dimensional and Material Specifications
Our production engineering strictly follows global dimensional codes to ensure hassle-free integration with global piping infrastructure and commercial boiler packages.
| Parameter |
Specification Details |
| Design Standards |
ASME B16.5, ASME B16.47 (Series A & B large diameter boundaries up to 60"), EN 1092-1 Type 05, DIN, JIS, BS 4504 |
| Material Specifications |
ASTM A105/A105N, ASTM A350 LF2, ASTM A694 (F42, F52, F60, F65, F70), ST 37.2, C22.8, P250GH |
| Pressure Classes |
Class 150, 300, 400, 600, 900, 1500, 2500 LBS / metric PN6 to PN400 parameters |
| Facing Design Formats |
Raised Face (RF Serrated), Flat Face (FF), Ring Type Joint (RTJ oval/octagonal groove ring) |
| Size Range Spectrum |
1/2” NB up to 60” NB (Full coverage to seal matching schedules from Sch 40 to Sch XXS) |
| Testing Regimens |
100% PMI analysis, Volumetric Ultrasonic Disk Check, CMM Geometric Audit, LPT, Hardness check |
Driving B2B Procurement via an Authorized Flanges Dealer in Mumbai
For global engineering, procurement, and construction (EPC) firms managing large-scale industrial projects, handling thousands of pipeline connections is a complex logistical task. Partnering with a dedicated distribution channel in Mumbai gives you a distinct operational edge.
We provide volume-based commercial discounts, comprehensive material traceability certifications (MTC EN 10204 3.1/3.2), and durable, sea-worthy packaging designed to prevent edge dents, rim distortion, or seating face scratches during transport. Additionally, our sales engineers provide direct technical support to procurement teams, verifying imperial bolt patterns, checking pressure class limits, and confirming material compatibility to match project parameters perfectly.
Carbon Steel Blind Flanges Exporter in Mumbai
Fulfilling Global Contracts as a Top Flanges Exporter from Mumbai
Our focus on precision machining and zero-defect forging has earned strong international trust. Operating from the export hub of Mumbai, we regularly ship high-reliability carbon steel blind flanges to chemical processing complexes in the Middle East, high-temperature power generation infrastructures in Europe, and water distribution networks across Southeast Asia.
Every export order passes through a strict final quality checkpoint, including full dimensional analysis, 100% PMI validation, and face flatness checks. We package shipments in heavy-duty, export-grade wooden cases equipped with moisture-resistant barriers and tailored face protectors. This ensures your components arrive at the project site ready for immediate installation.
Technical Specifications Summary
| Carbon Steel Blind Flanges – Technical Specifications |
Details |
| Size Range Spectrum |
1/2" to 60" (Complete Nominal Bore Spectrum for line terminations) |
| Pressure Designation |
150#, 300#, 400#, 600#, 900#, 1500#, 2500# LBS, metric PN 6 to PN 400 Bar ratings |
| Configuration Options |
Solid Standard Raised Face Blind (BLRF), Flat Face Blind (FF), Tapped Blind, Spectacle Blind, Paddle Blank |
| Face Design Formats |
Raised Face (Serrated RF), Flat Face (FF), Ring Type Joint (RTJ Groove), Tongue & Groove |
| Manufacturing Process |
100% Forged / Fully Heat Treated & Precision CNC Turned Face Machined Finished |
| Testing Protocols |
PMI verification, Brinell Hardness check, Volumetric Ultrasonic Disk Audit, LPT, Face Flatness checking |
| Surface Protection |
Anti-Rust Oiled, Black Phosphated, Zinc Electroplated, Hot-Dip Galvanizing, Lacquer Coating |