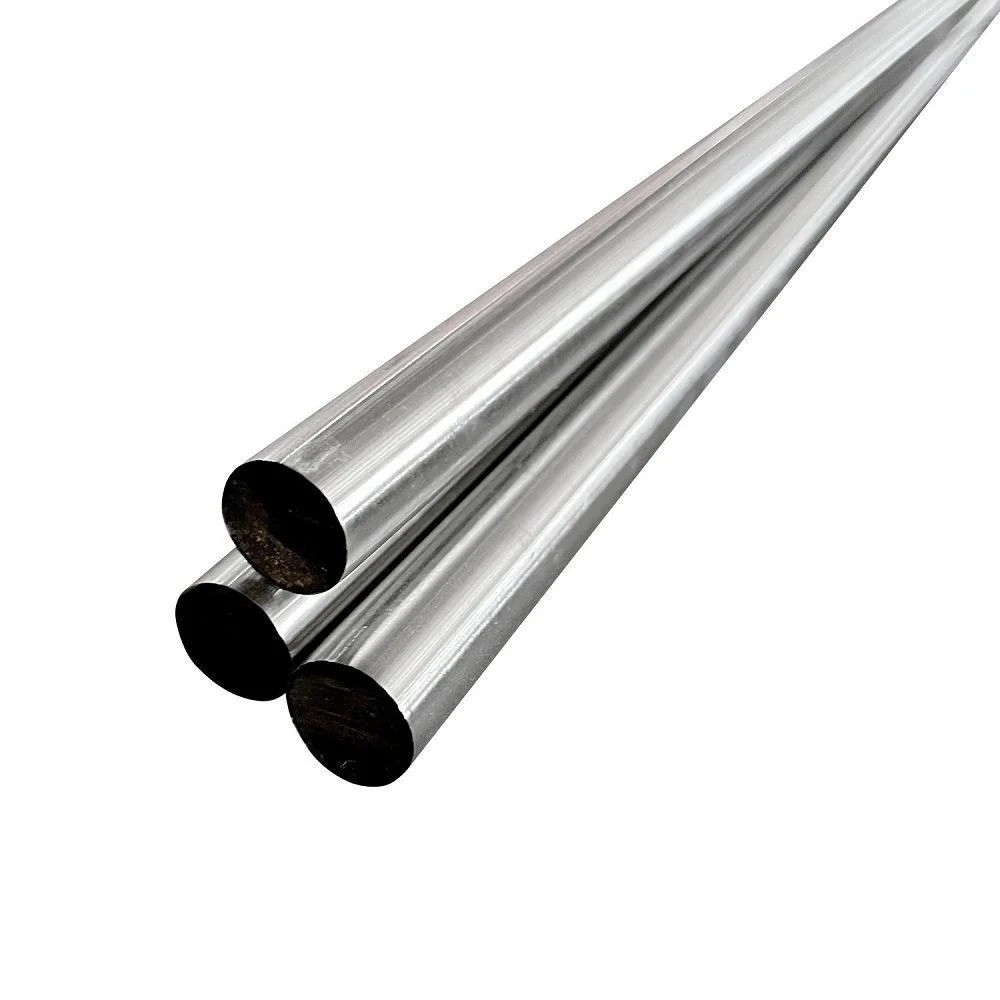
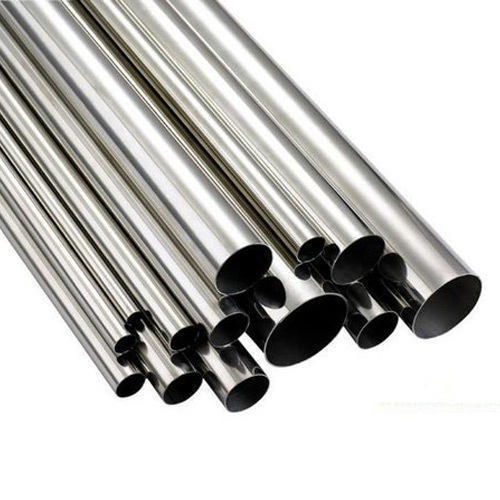
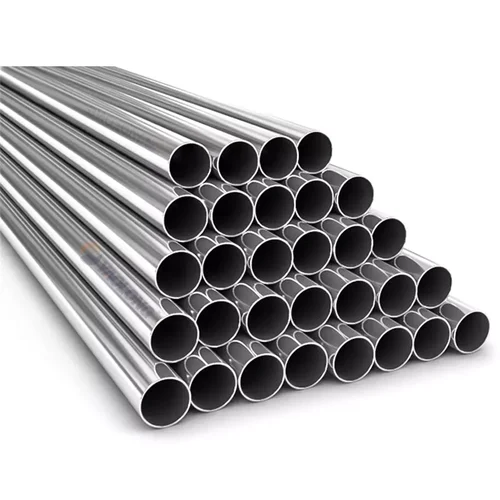
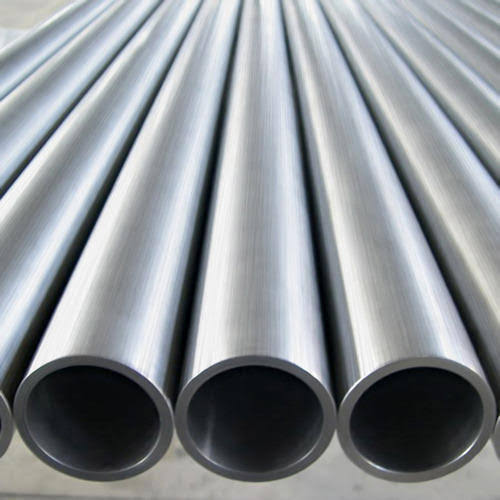
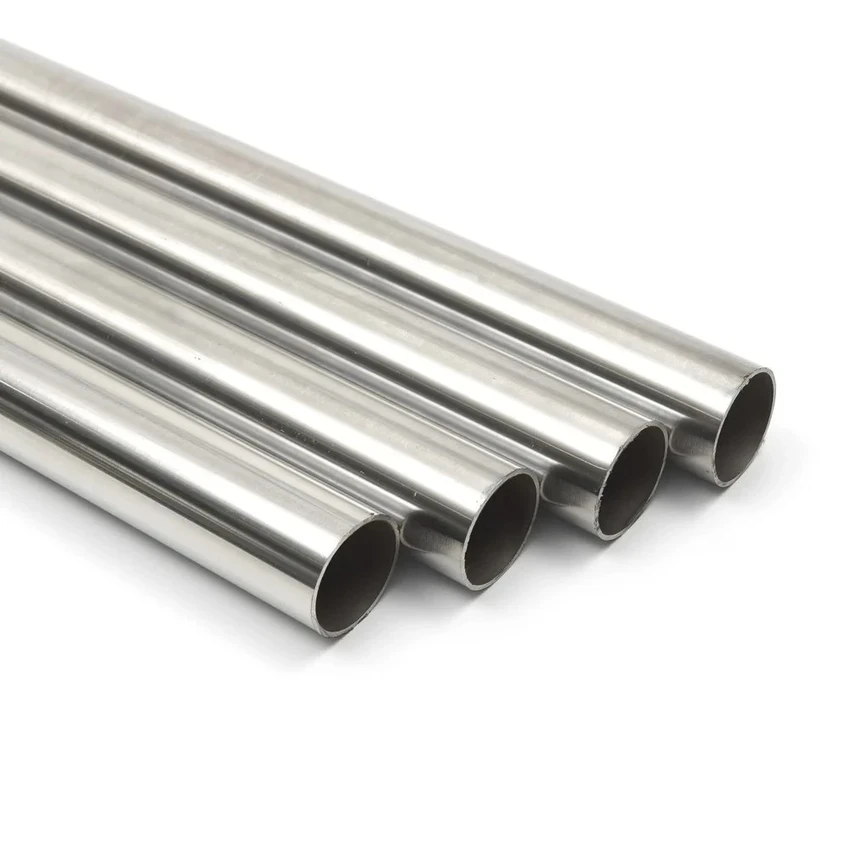
304H Stainless Steel Tubes Supplier in Mumbai
The Metallurgy and Structural Classification Matrix
The operational lifespan, mechanical resilience, and thermal efficiency of a 304H stainless steel tube depend entirely on its specific chemical composition and its primary structural classification.
Chemical Composition Matrix (UNS S30400 vs UNS S30409) (%)
The chemical formulation of Grade 304H is precisely balanced to deliver robust high-temperature yield strength and structural durability:
| Grade Type |
Chromium (Cr) |
Nickel (Ni) |
Carbon (C) |
Manganese (Mn) |
Silicon (Si) |
Phosphorus (P) |
Sulfur (S) |
| Standard 304 |
18.00–20.00 |
8.00–10.50 |
0.08 Max |
2.00 Max |
0.75 Max |
0.045 Max |
0.030 Max |
| 304H (High-Carbon) |
18.00–20.00 |
8.00–10.50 |
0.04–0.10 |
2.00 Max |
0.75 Max |
0.045 Max |
0.030 Max |
Note: The "H" designation explicitly requires a carbon range of 0.04% to 0.10%. This elevated carbon threshold is what gives 304H its superior long-term creep strength and mechanical fatigue resistance compared to standard low-carbon 304L or standard 304 variants at extreme continuous operating thermal boundaries.
Seamless vs. Welded 304H Stainless Tubing Classifications
Depending on specific structural constraints, pressure ratings, and economic parameters, we supply 304H stainless steel tubing across two primary configurations:
| Parameter |
Seamless Tubing (ASTM A213) |
Welded Tubing (ASTM A249) |
| Manufacturing Process |
Extruded from solid forged billets, followed by cold-drawing or pilgering. Completely weld-free. |
Formed from continuous precision strip-steel, welded using automated TIG/Plasma arc protocols without filler metal. |
| Pressure Thresholds |
Substantially higher burst pressure profiles; completely eliminates the risk of directional seam failure. |
Moderate pressure ratings; typically restricted by a structural joint efficiency factor (e.g., 0.85 or 1.00 for fully radiographed lines). |
| Dimensional Tolerances |
Excellent, though slight wall concentricity variations can occur over long structural lengths. |
Ultra-precise wall thickness uniformity, as the starting point is a high-accuracy rolled steel sheet or strip. |
| Primary Applications |
High-pressure power utility boilers, radiant superheaters, heat exchanger bundles, and heavy petrochemical reactors. |
Commercial cooling coils, high-temperature exhaust loops, heat exchangers, and furnace cabinetry. |
Primary Industrial Tubing Formats and Applications
Depending on the required fluid velocity, spatial limitations, and target heat transfer coefficients, we supply specialized tubing profiles:
- Heat Exchanger & Condenser Tubes: Straight precision lengths explicitly optimized for thin-wall thermal transmittance, designed for seamless rolling or orbital welding into heavy tubesheet matrices.
- U-Bent Tubing: High-purity straight tubes precision-bent into customized U-profiles, solution-annealed along the bend radius to relieve stress, and pre-tested for immediate installation in shell-and-tube configurations.
- Boiler & Superheater Tubes: Precise, heavy-wall tubing designed to withstand harsh structural loading, internal steam pressures, and severe continuous thermal exposure inside utility power boilers.
Dimensional and Material Specifications
Our production engineering strictly follows global dimensional codes to ensure hassle-free integration with global piping infrastructure and commercial industrial systems.
| Parameter |
Specification Details |
| Design Standards |
ASTM A213 (Seamless Ferritic and Austenitic Alloy-Steel Boiler, Superheater, and Heat-Exchanger Tubes), ASTM A249 (Welded Boiler/Heat-Exchanger), EN 10216-5, DIN 17458 |
| Material Specifications |
High-Carbon Austenitic Stainless Steel Grade 304H (UNS S30409 / W.Nr. 1.4948) |
| Size Specification Matrix |
1/8” OD up to 4” OD standard range (Wall thickness coverage spanning 0.020” up to 0.500” / SWG or BWG parameters) |
| Surface Finish Options |
Bright Annealed (BA), Mill Finish, Pickled & Annealed (AP), Polished Grit finishes (180, 240, 320, 400 Mirror) |
| Testing Regimens |
100% PMI verification, Eddy Current (ECT), Hydrostatic Containment, Flaring & Flattening tests, Ultrasonic thickness checks |
Driving B2B Procurement via an Authorized Tubes Dealer in Mumbai
For global engineering, procurement, and construction (EPC) firms, original equipment manufacturers (OEMs), and thermal facility builders handling intense high-temperature environments, sourcing fully traceable tubing is essential. Partnering with a dedicated distribution channel in Mumbai gives you a distinct operational edge.
We provide volume-based commercial discounts, comprehensive material traceability certifications (MTC EN 10204 3.1/3.2), and durable, sea-worthy packaging designed to prevent bending, wall scratching, or end deformation during transport. Tubes are packed in robust wooden crates with individual protective sleeve covers, ensuring your high-precision components arrive at the project site ready for immediate installation.
304H Stainless Steel Tubes Exporter in Mumbai
Fulfilling Global Contracts as a Top Precision Tubing Exporter from Mumbai
Our focus on precision drawing control and zero-defect quality validation has earned strong international trust. Operating from the export hub of Mumbai, we regularly ship high-reliability seamless and welded 304H stainless steel tubes to high-temperature furnace manufacturing networks in Europe, specialized refinery grids in the Middle East, and power generation installations across Southeast Asia.
Every export order passes through a strict final quality checkpoint, including full dimensional analysis, 100% PMI validation, and Eddy Current testing verification. We package shipments in heavy-duty, export-grade boxes and palletized crates equipped with protective internal formatting and moisture-resistant vapor barriers. This ensures your high-precision components arrive at the project site in perfect operational condition.
Technical Specifications Summary
| 304H Stainless Tubing – Technical Specifications |
Details |
| Outside Diameter Range |
1/8" to 4" (3.17 mm to 101.6 mm) standard nominal spectrum |
| Wall Thickness Range |
0.020" to 0.500" (Custom dimensions matching SWG / BWG wall schedules) |
| Type Configurations |
Seamless Cold-Drawn Tubes, Welded TIG/Plasma Tubes, U-Bent Condenser Tubes, Straight Boiler Tubes |
| Surface Condition Formats |
Bright Annealed (BA), Descaled Pickled (AP), Mechanical Polished Finish (up to 400 Grit) |
| Manufacturing Standards |
100% Cold-Pilgered / Cold-Drawn & Controlled Atmosphere Heat Treated |
| Testing Protocols |
Eddy Current Testing (ECT), Hydrostatic Proofing, Flaring, Flattening, Hardness, Grain Size Verification |
| Certification Scope |
EN 10204 3.1 / 3.2 Mill Test Certificate, Compliance with NACE MR0175 / Sour Service parameters |