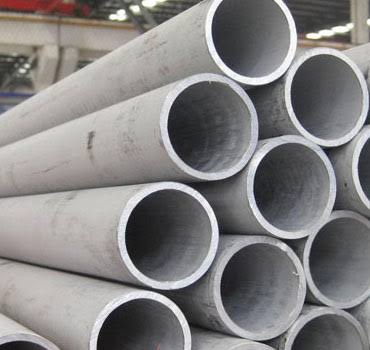
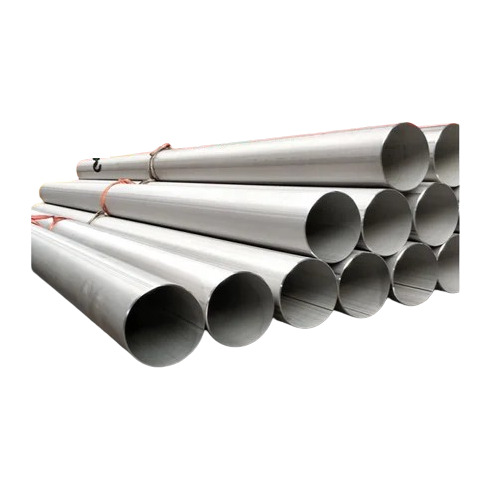
Hastelloy B2 Pipes Supplier in Mumbai
The Metallurgy and Primary Structural Classification Matrix
The operational lifespan, mechanical resilience, and chemical defense of an industrial Hastelloy B2 pipe depend entirely on its specific chemical composition and its primary structural classification.
Chemical Composition Matrix (UNS N10665) (%)
The chemical formulation of Grade B2 is precisely regulated to deliver complete immunity to boiling hydrochloric acid under strictly reducing boundaries:
| Nickel (Ni) |
Molybdenum (Mo) |
Iron (Fe) |
Chromium (Cr) |
Cobalt (Co) |
Carbon (C) |
Manganese (Mn) |
Silicon (Si) |
Phosphorus (P) |
Sulfur (S) |
| Balance |
26.00–30.00 |
2.00 Max |
1.00 Max |
1.00 Max |
0.02 Max |
1.00 Max |
0.10 Max |
0.04 Max |
0.03 Max |
Note: Hastelloy B2 is explicitly formulated with ultra-low carbon (0.02% max) and iron to resist the formation of grain-boundary carbide precipitates in the weld heat-affected zone (HAZ). However, because it lacks chromium, it must never be deployed in process streams containing oxidizing contaminants (such as ferric ions, cupric ions, or dissolved oxygen), which cause rapid, catastrophic accelerated corrosion.
Seamless vs. Welded Hastelloy B2 Piping Structural Matrix
Depending on line dimensions, operating pressure class parameters, and system requirements, we supply industrial Hastelloy B2 piping across two foundational configurations:
| Parameter |
Seamless Pipe (ASTM B622) |
Welded Pipe (ASTM B619 / B626) |
| Manufacturing Method |
Hot-extruded and cold-pilgered from solid forged nickel alloy billets. Features an uninterrupted solid cylinder wall structure without welds. |
Formed from continuous precision strip or plate, welded longitudinally via automated TIG/Plasma arc lines without filler metal. |
| Pressure Capabilities |
Maximum hydrostatic retention; completely eliminates the risk of directional seam failure under severe chemical loads. |
Moderate to high pressure; governed by a joint efficiency factor ($E = 0.85$ or $1.00$ based on volumetric NDT status). |
| Size Range Spectrum |
Standard availability typically restricted from 1/2" NB up to 8" NB due to heavy hydraulic extrusion limits of this high-moly alloy. |
Virtually unrestricted; ideal for large-diameter process lines stretching from 1/2" NB up to 24" NB and above. |
| Wall Thickness Uniformity |
Excellent, though slight wall concentricity variations can occur over long structural lengths. |
Ultra-precise wall thickness uniformity, as the starting point is a high-accuracy rolled nickel sheet or strip. |
Primary Dimensional Specifications and Wall Thickness Schedules
Our production engineering strictly follows global dimensional codes to ensure hassle-free integration with global piping infrastructure, valves, flanges, and fittings.
| Parameter |
Specification Details |
| Design Standards |
ASME B36.10M (Welded and Seamless Wrought Steel Pipe dimensional parity), ASME B36.19M (Stainless and Corrosion Resistant Pipe standards), DIN, ISO, EN standards |
| Material Specifications |
ASTM B622 (Seamless Nickel-Alloy Pipe), ASTM B619 (Welded Nickel-Alloy Pipe), ASTM B626 (Welded and Co-Drawn Pipe), EN 10216-5 |
| Common Material Grades |
Hastelloy B2 (UNS N10665 / W.Nr. 2.4617) |
| Wall Thickness Schedules |
Sch 5S, Sch 10S, Sch 40S (Standard Wall / STD), Sch 80S (Extra Heavy / XS), Sch 160, Sch XXS (Double Extra Strong) |
| Facing End Layouts |
Beveled Ends (BE standard for butt-welding), Plain Ends (PE for socket-welding or slip-on layouts), Threaded Ends (TE matching NPT criteria) |
| Size Specification Matrix |
1/2” NB up to 24” NB standard coverage (Custom wall dimensions and large-diameter pipelines executed to blueprint criteria) |
| Testing Regimens |
100% PMI verification, Hydrostatic Leak Containment, Volumetric Ultrasonic/Radiographic Seam Check, Hardness check, Intergranular Corrosion Checking |
Driving B2B Procurement via an Authorized Pipes Dealer in Mumbai
For global engineering, procurement, and construction (EPC) firms, plant turnaround contractors, and infrastructure developers handling high-volume reducing networks, sourcing traceably certified industrial Hastelloy pipelines is a precise task. Partnering with a dedicated distribution channel in Mumbai gives you a distinct operational edge.
We provide volume-based commercial discounts, comprehensive material traceability certifications (MTC EN 10204 3.1/3.2), and durable, sea-worthy bundling packaging designed to prevent transit surface scratches, end bevel distortion, or bending. Pipes are protected with external anti-corrosion wrappers and end plastic caps, ensuring your components arrive at the project site ready for immediate welding and installation.
Hastelloy B2 Pipes Exporter in Mumbai
Fulfilling Global Contracts as a Top Core Piping Exporter from Mumbai
Our focus on precision dimensional control and zero-defect quality validation has earned strong international trust. Operating from the export hub of Mumbai, we regularly ship high-reliability seamless and welded Hastelloy B2 pipes to severe chemical synthesis units in the Middle East, specialized acid processing infrastructures in Europe, and industrial processing operations across Southeast Asia.
Every export order passes through a strict final quality checkpoint, including full dimensional analysis, 100% PMI validation, and hydrostatic proofing checks. We package shipments in heavy-duty, seaworthy bundles or wooden crates equipped with moisture-resistant barriers and protective end protectors. This ensures your high-yield components arrive at the project site ready for immediate installation.
Technical Specifications Summary
| Hastelloy B2 Industrial Piping – Technical Specifications |
Details |
| Size Specification Range |
1/2" to 24" (Complete Nominal Bore Spectrum for pure reducing fluid containment) |
| Wall Thickness Range |
Sch 5S up to Sch XXS (Complete coverage from thin-wall utility to ultra-heavy high-pressure wall schedules) |
| Type Configurations |
Seamless Hot-Extruded & Cold-Pilgered Pipe, Longitudinally Welded (TIG/Plasma) Pipe |
| End Finish Formats |
Weld Beveled Ends (37.5° Bevel Angle), Square Cut Plain Ends, Male Threaded Ends (NPT) |
| Surface Protection Options |
Cleaned Mill Finish, Bright Annealed (BA), Protective PE Wrap, End Cap Containment |
| Testing Protocols |
Hydrostatic Leak Containment, Radiographic/Ultrasonic Seam Audit, PMI analysis, Flattening & Bend tests, Hardness verification |
| Certification Parity |
EN 10204 3.1 / 3.2 Mill Test Certification, Compliance with NACE MR0175 / Sour Service parameters |