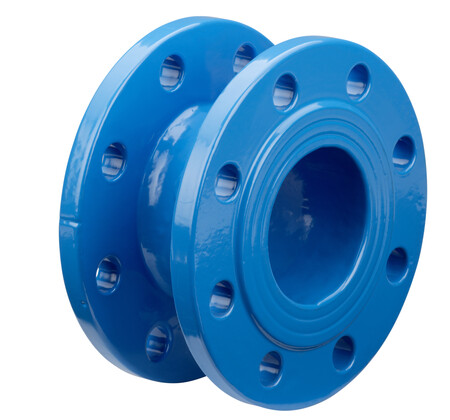
ASA Flanges Supplier in Mumbai
The Metallurgy and Legacy Pressure Designation Engineering
The industrial operational lifespan of a heavy-duty ASA flange is determined by its specific metallurgical composition and the precision of its sealing face machining.
Diverse Material Metallurgy and Environmental Performance
Industrial fluid routing demands a broad spectrum of material categories tailored to specific chemical and thermal conditions. Our production includes standard Carbon Steels (ASTM A105, IS 2062) providing high-tensile properties for ambient water or utility grids, and Low-Temperature Carbon Steel (ASTM A350 LF2) engineered to maintain exceptional notch toughness down to -46°C. For corrosive loops, we process Austenitic Stainless Steels (304/304L, 316/316L) which rely on a rich chromium-nickel blend to form an immediate, self-healing passive oxide layer. For advanced applications, we forge customized legacy dimensions from Duplex, Super Duplex, and high-temp Cr-Mo alloy steels.
Decoding ASA Historical Pressure Classes (ASA 150 vs. ASA 300)
Historically, the American Standards Association laid down the baseline pressure-temperature ratings that map directly onto contemporary ASME guidelines:
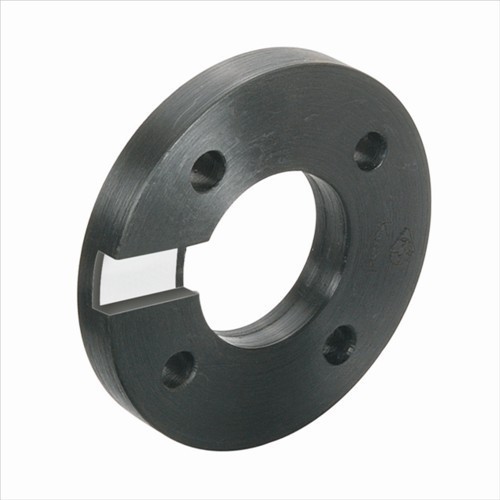
- ASA 150 Flanges: The standard low-to-medium pressure utility series designed with identical bolt patterns to modern ASME B16.5 Class 150#, serving general water, oil, and gas distribution lines.
- ASA 300 Flanges: A heavy-duty, thicker configuration featuring a larger bolt circle array, engineered to handle elevated operational pressures matching contemporary Class 300# structural standards.
Primary Body Configurations and Structural Joint Styles
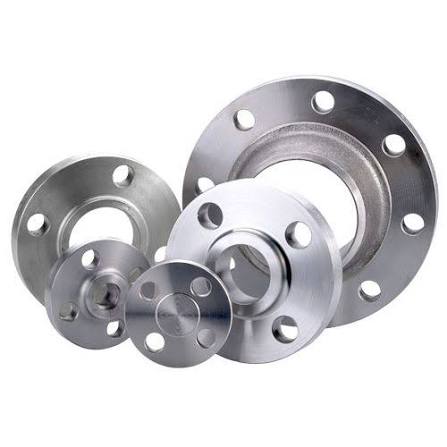
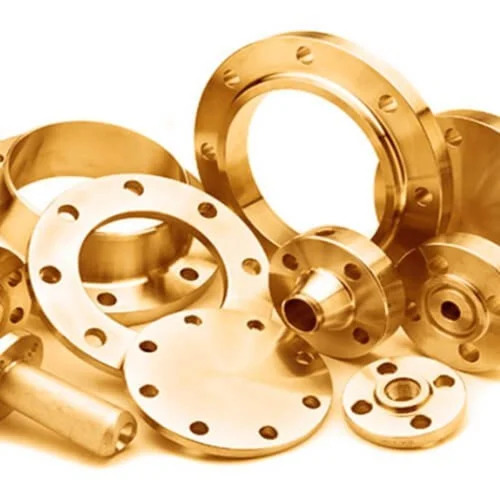
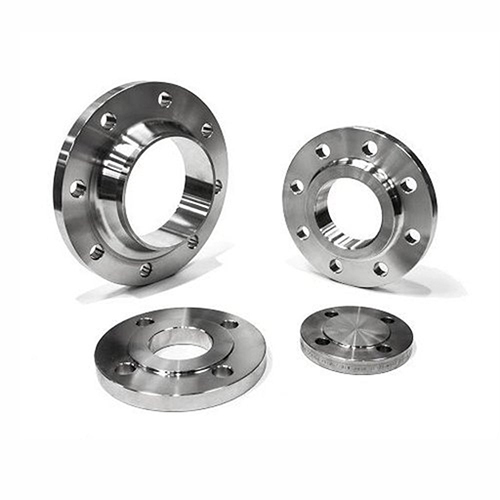
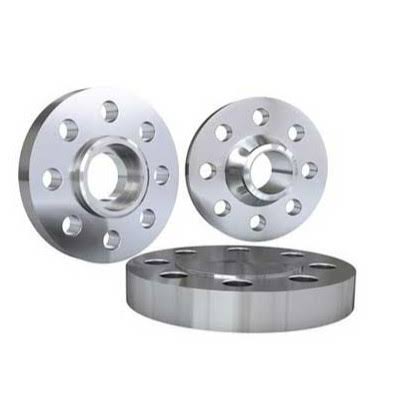
Depending on the system's velocity layout, internal pressure surges, and field installation parameters, we manufacture a complete line of body configurations:
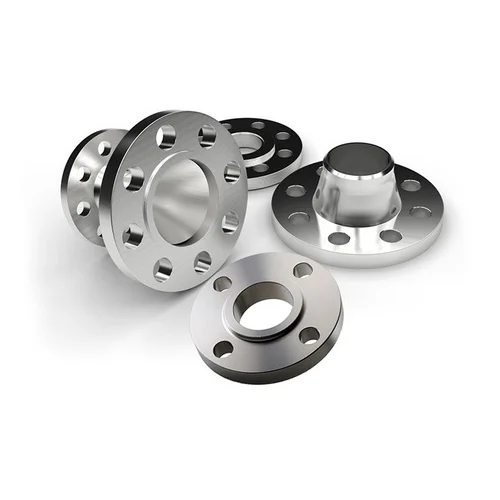
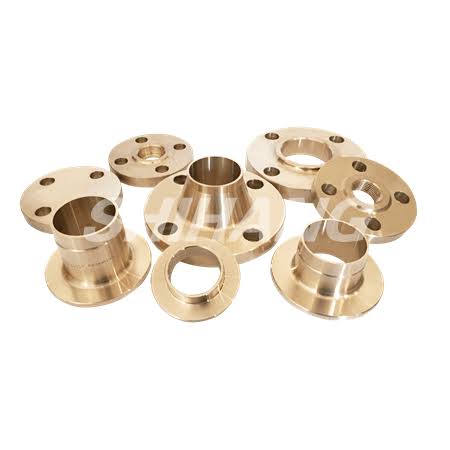
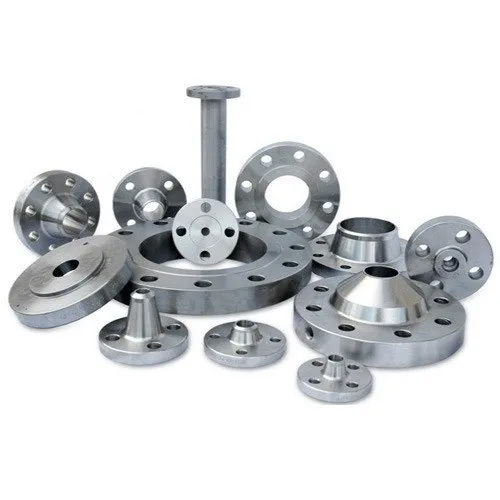
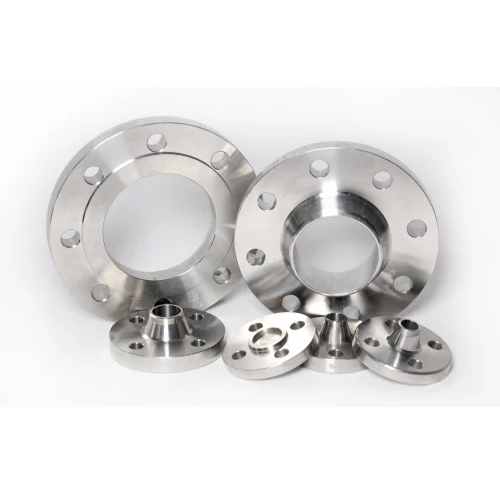
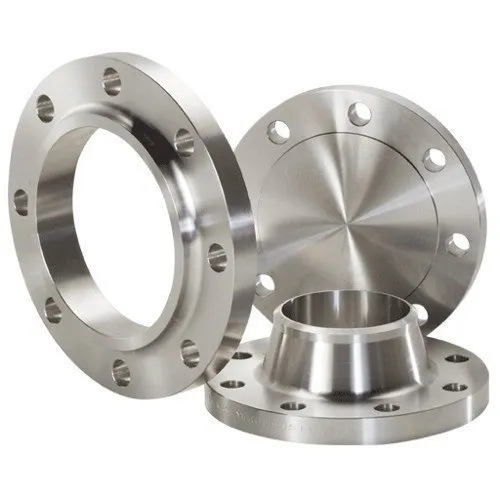
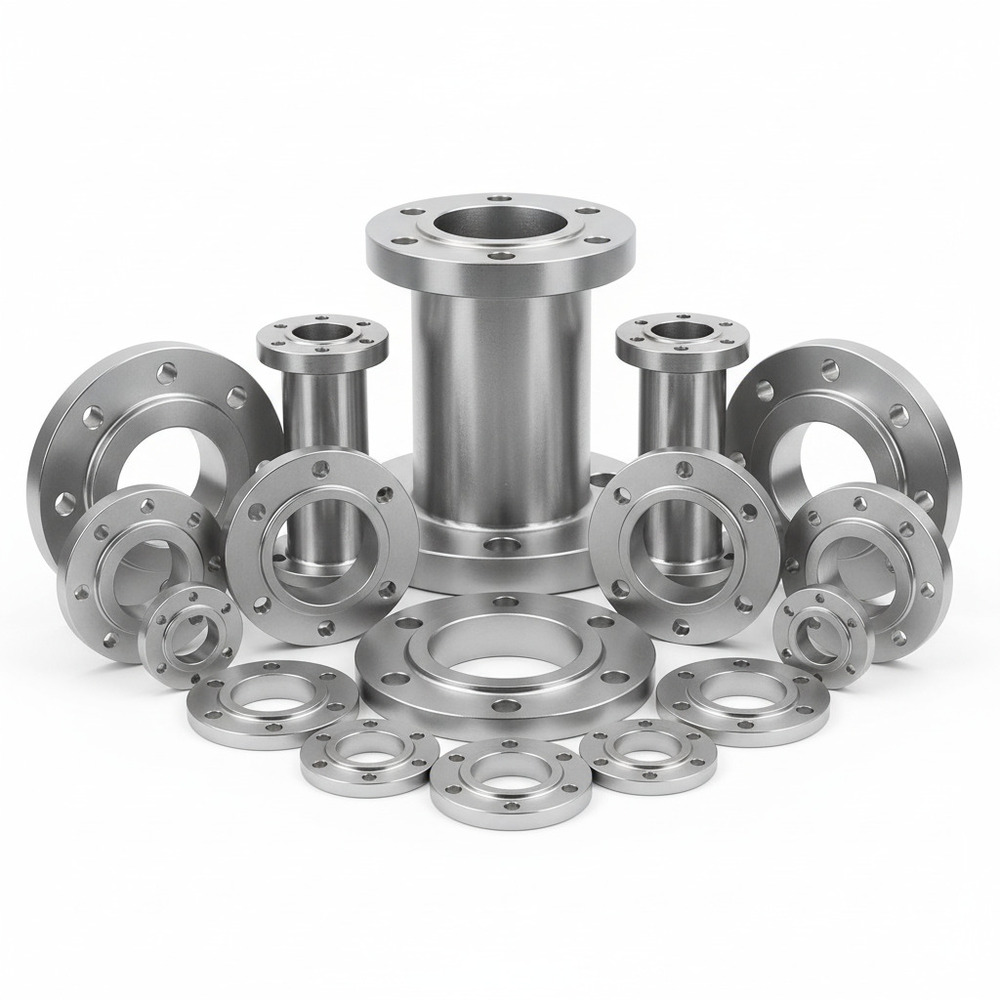
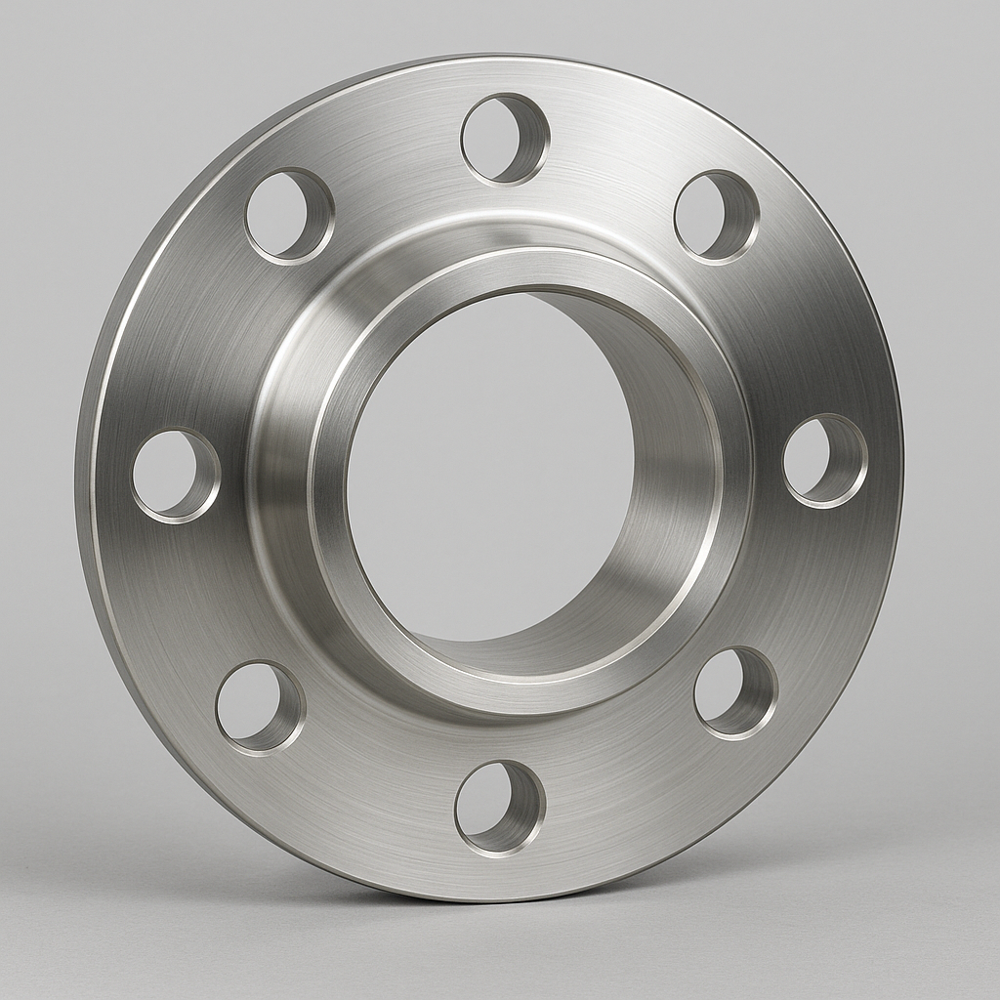
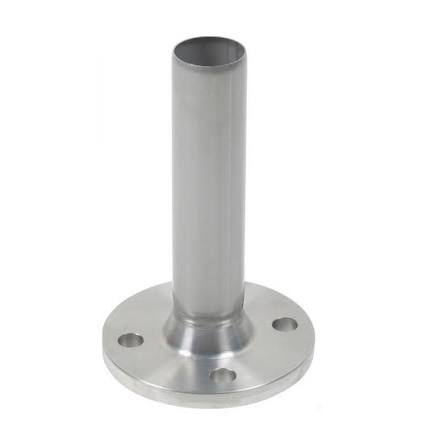
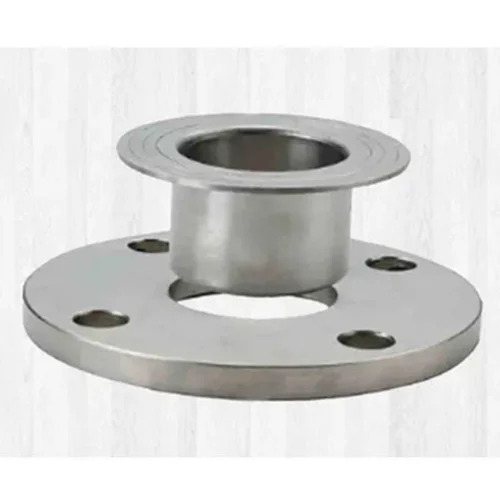
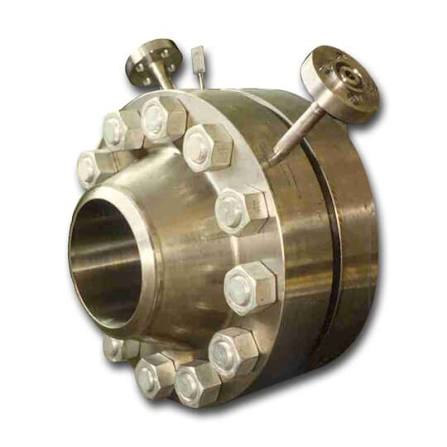
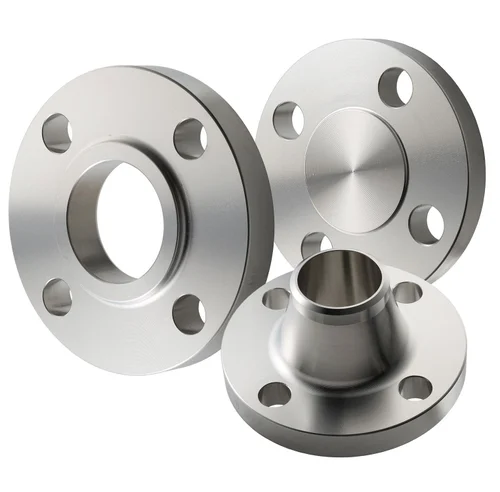
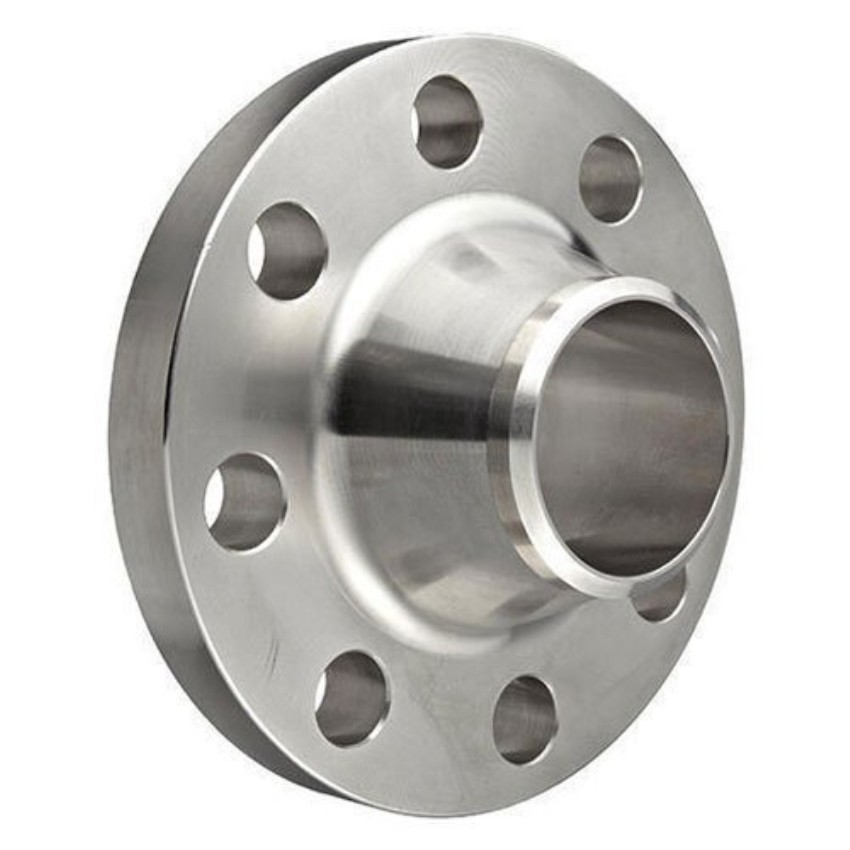
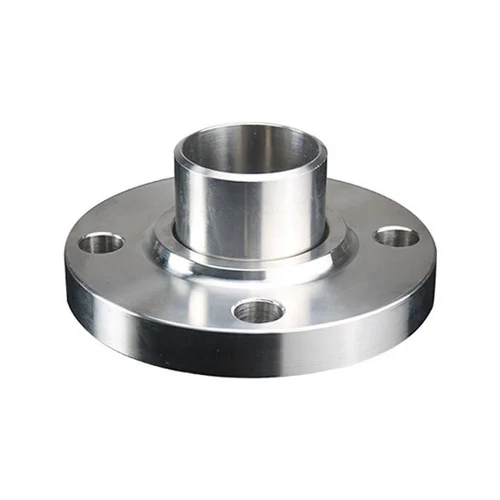
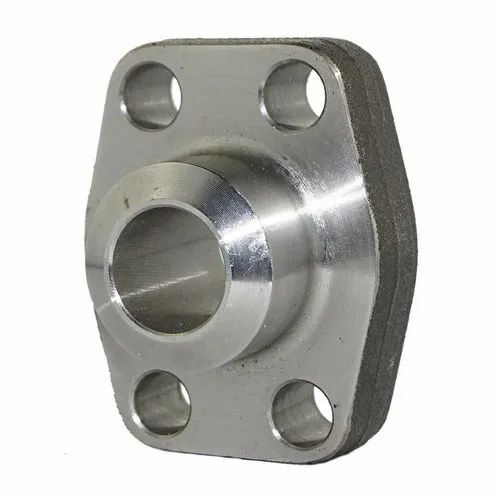
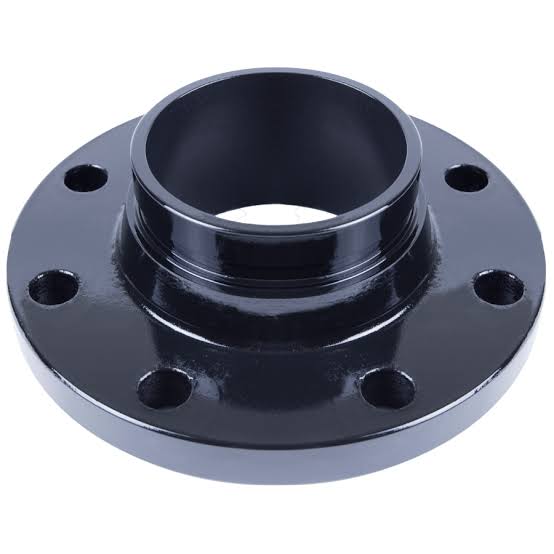
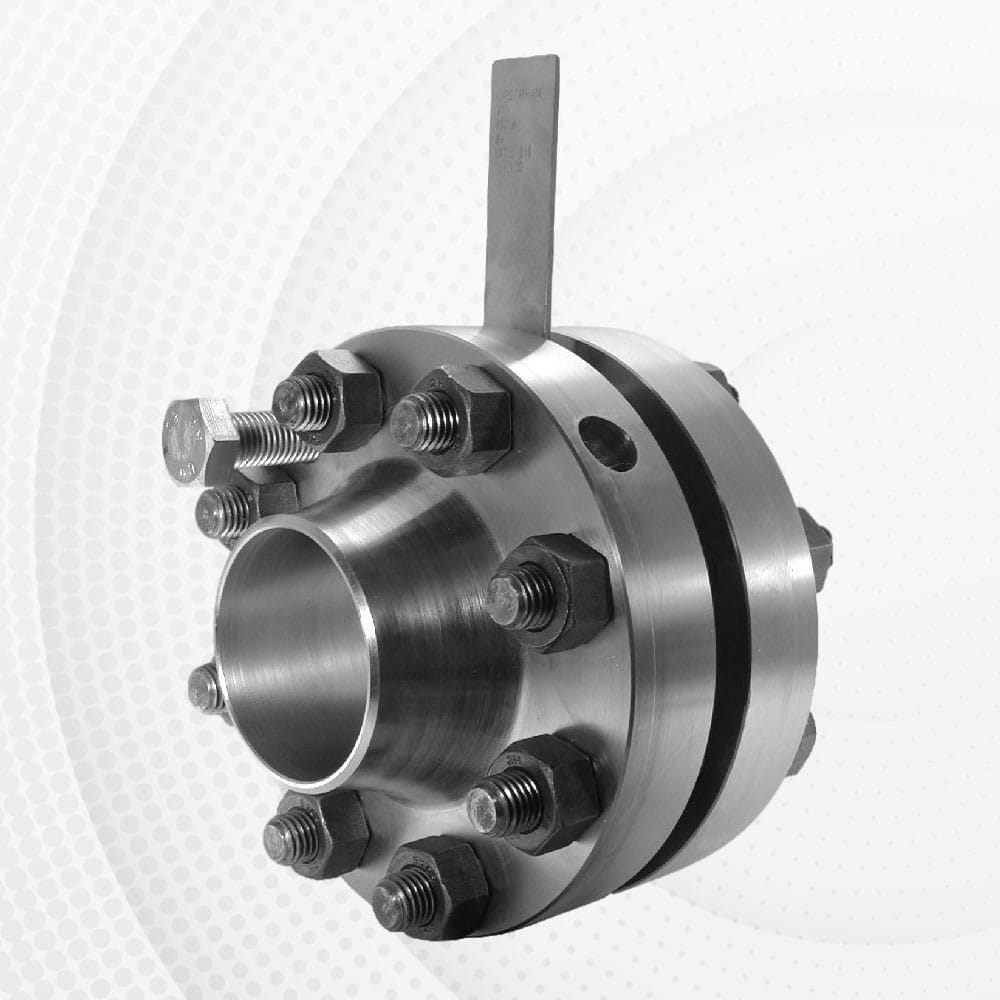
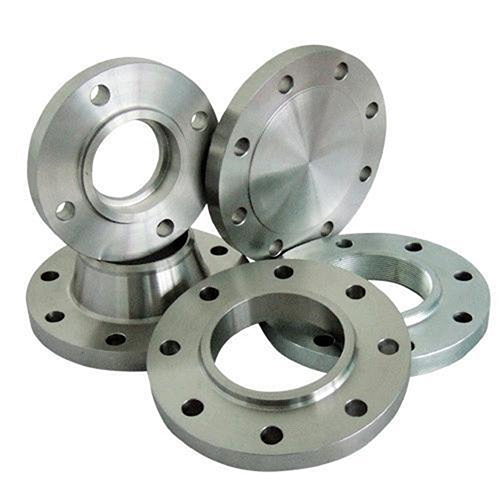
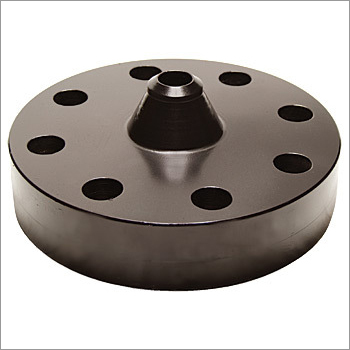
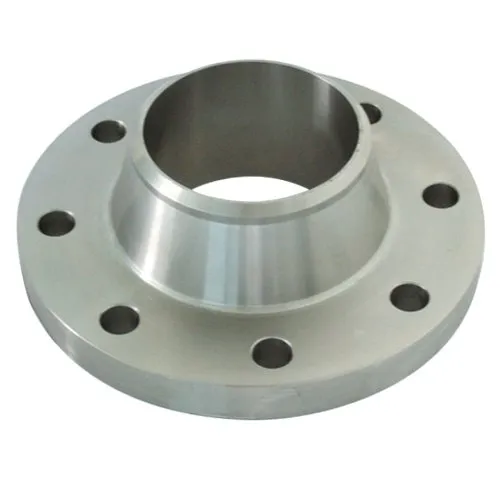
- ASA Weld Neck Flange (WN): Features a long, tapered structural hub that mirrors the pipe's internal schedule, shifting mechanical stress directly into the line. It is ideal for high-pressure or high-vibration legacy manifolds.
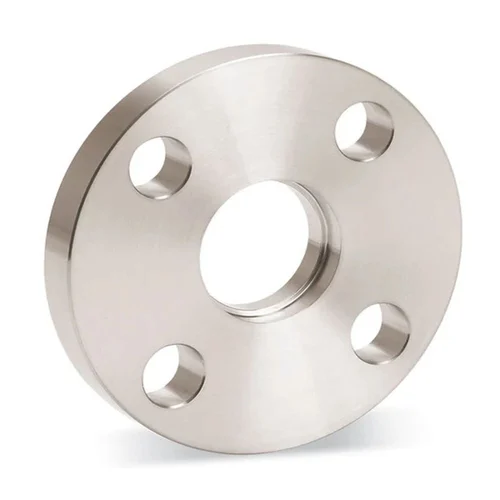
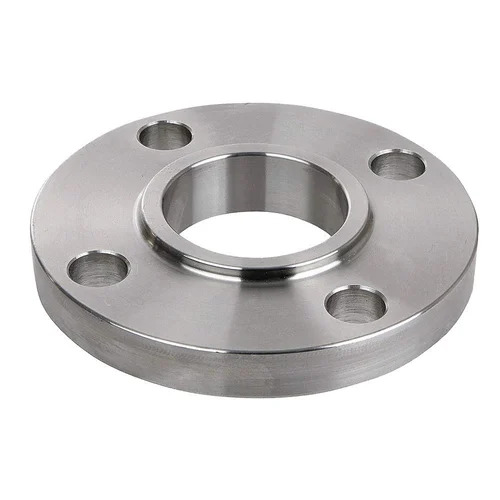
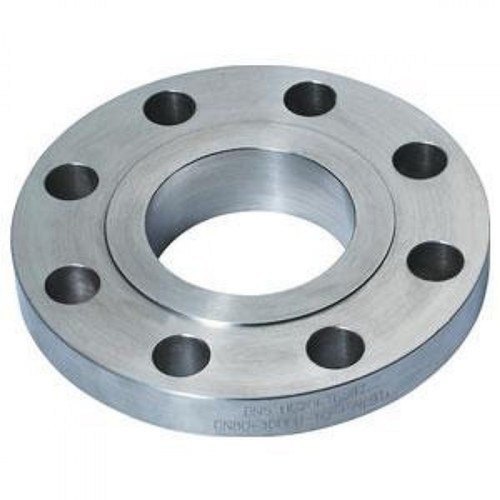
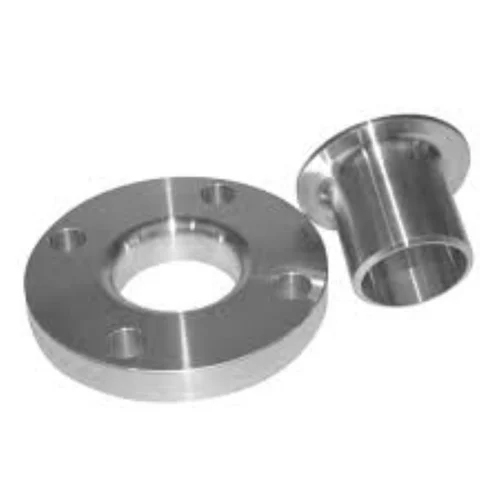
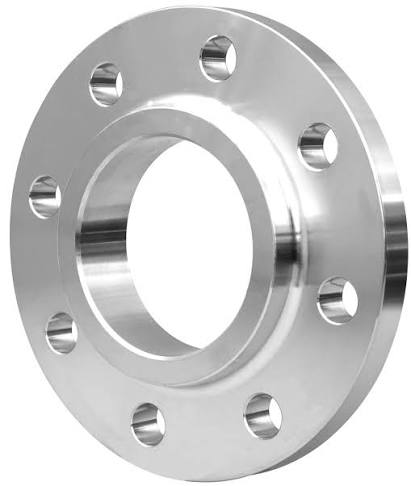
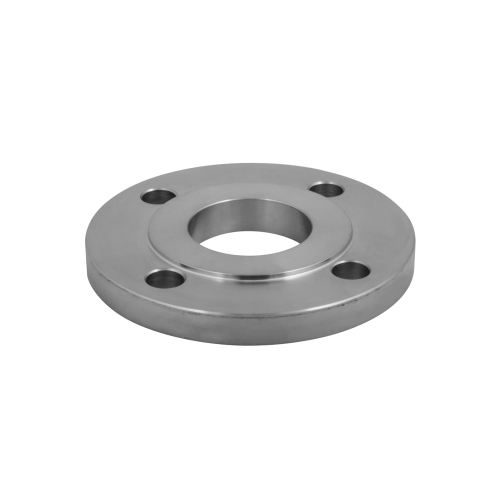
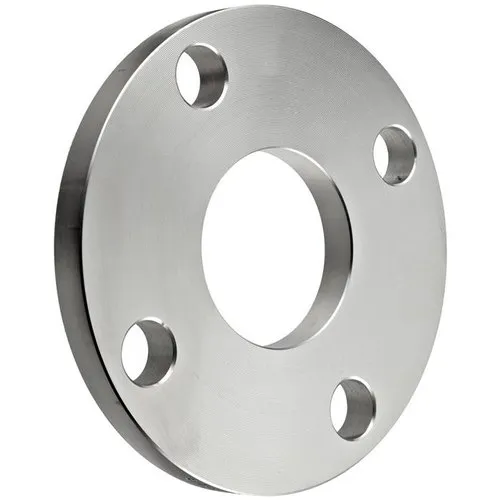
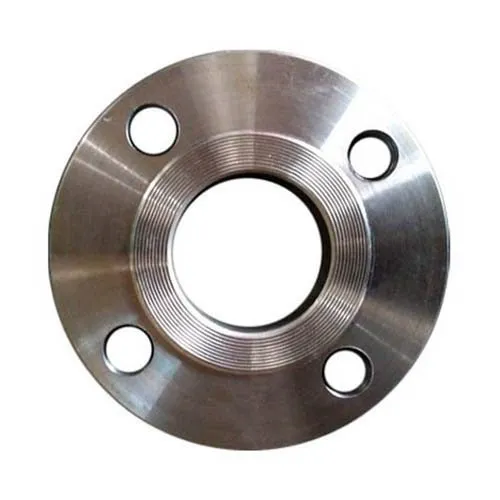
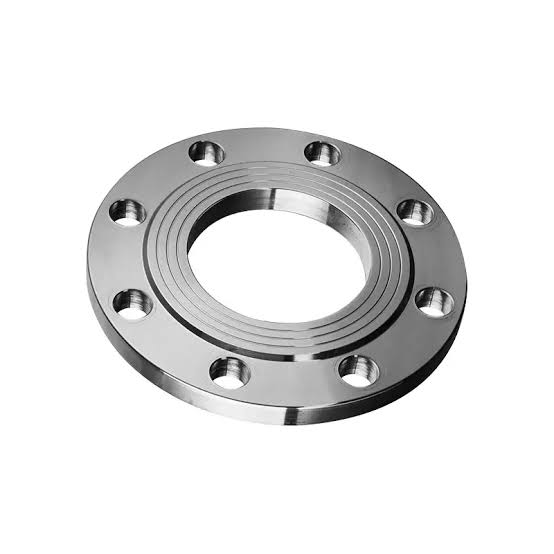
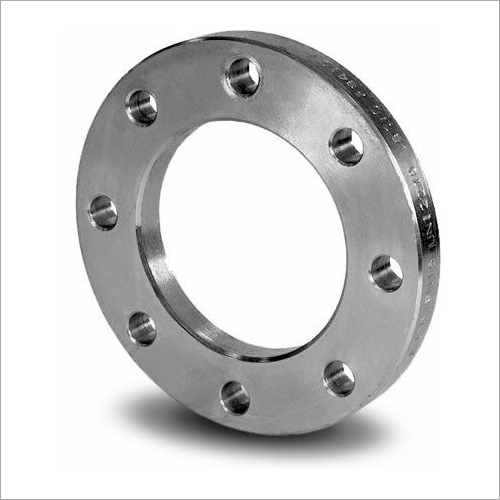
- ASA Slip-On Flange (SO): Slides easily over the outside diameter of the pipe and is secured with dual internal and external structural fillet welds, making it highly cost-effective and straightforward to align in standard processing lines.
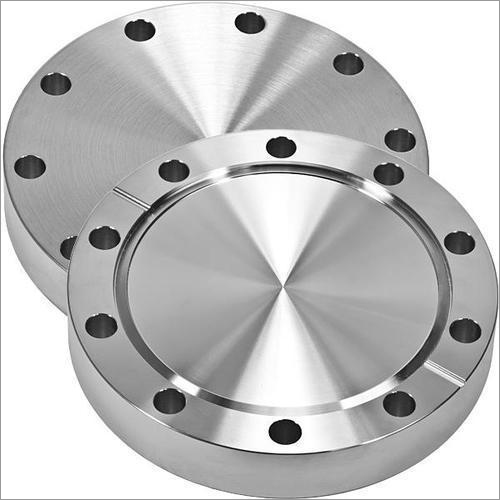
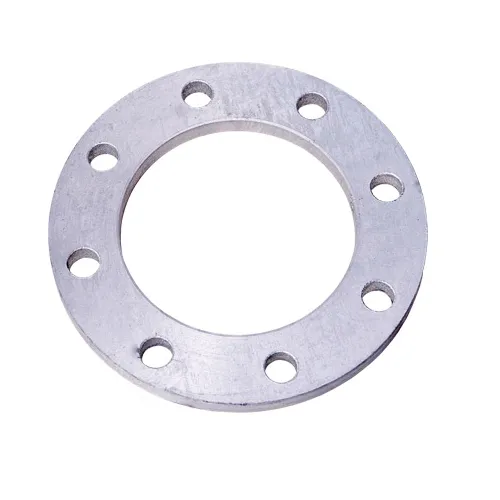
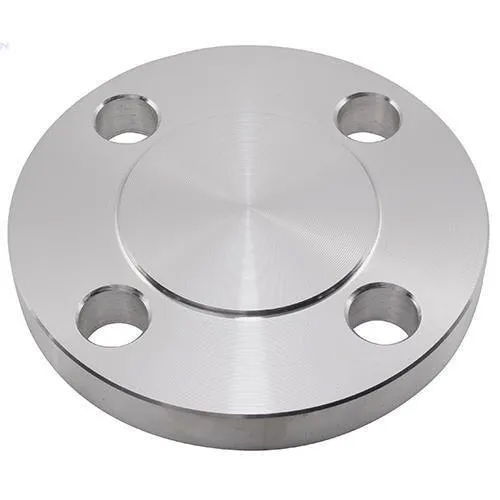
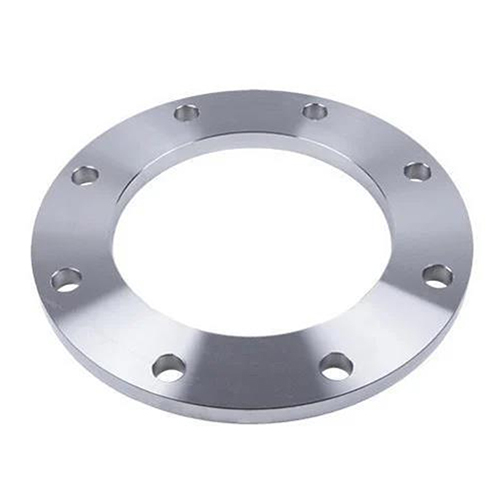
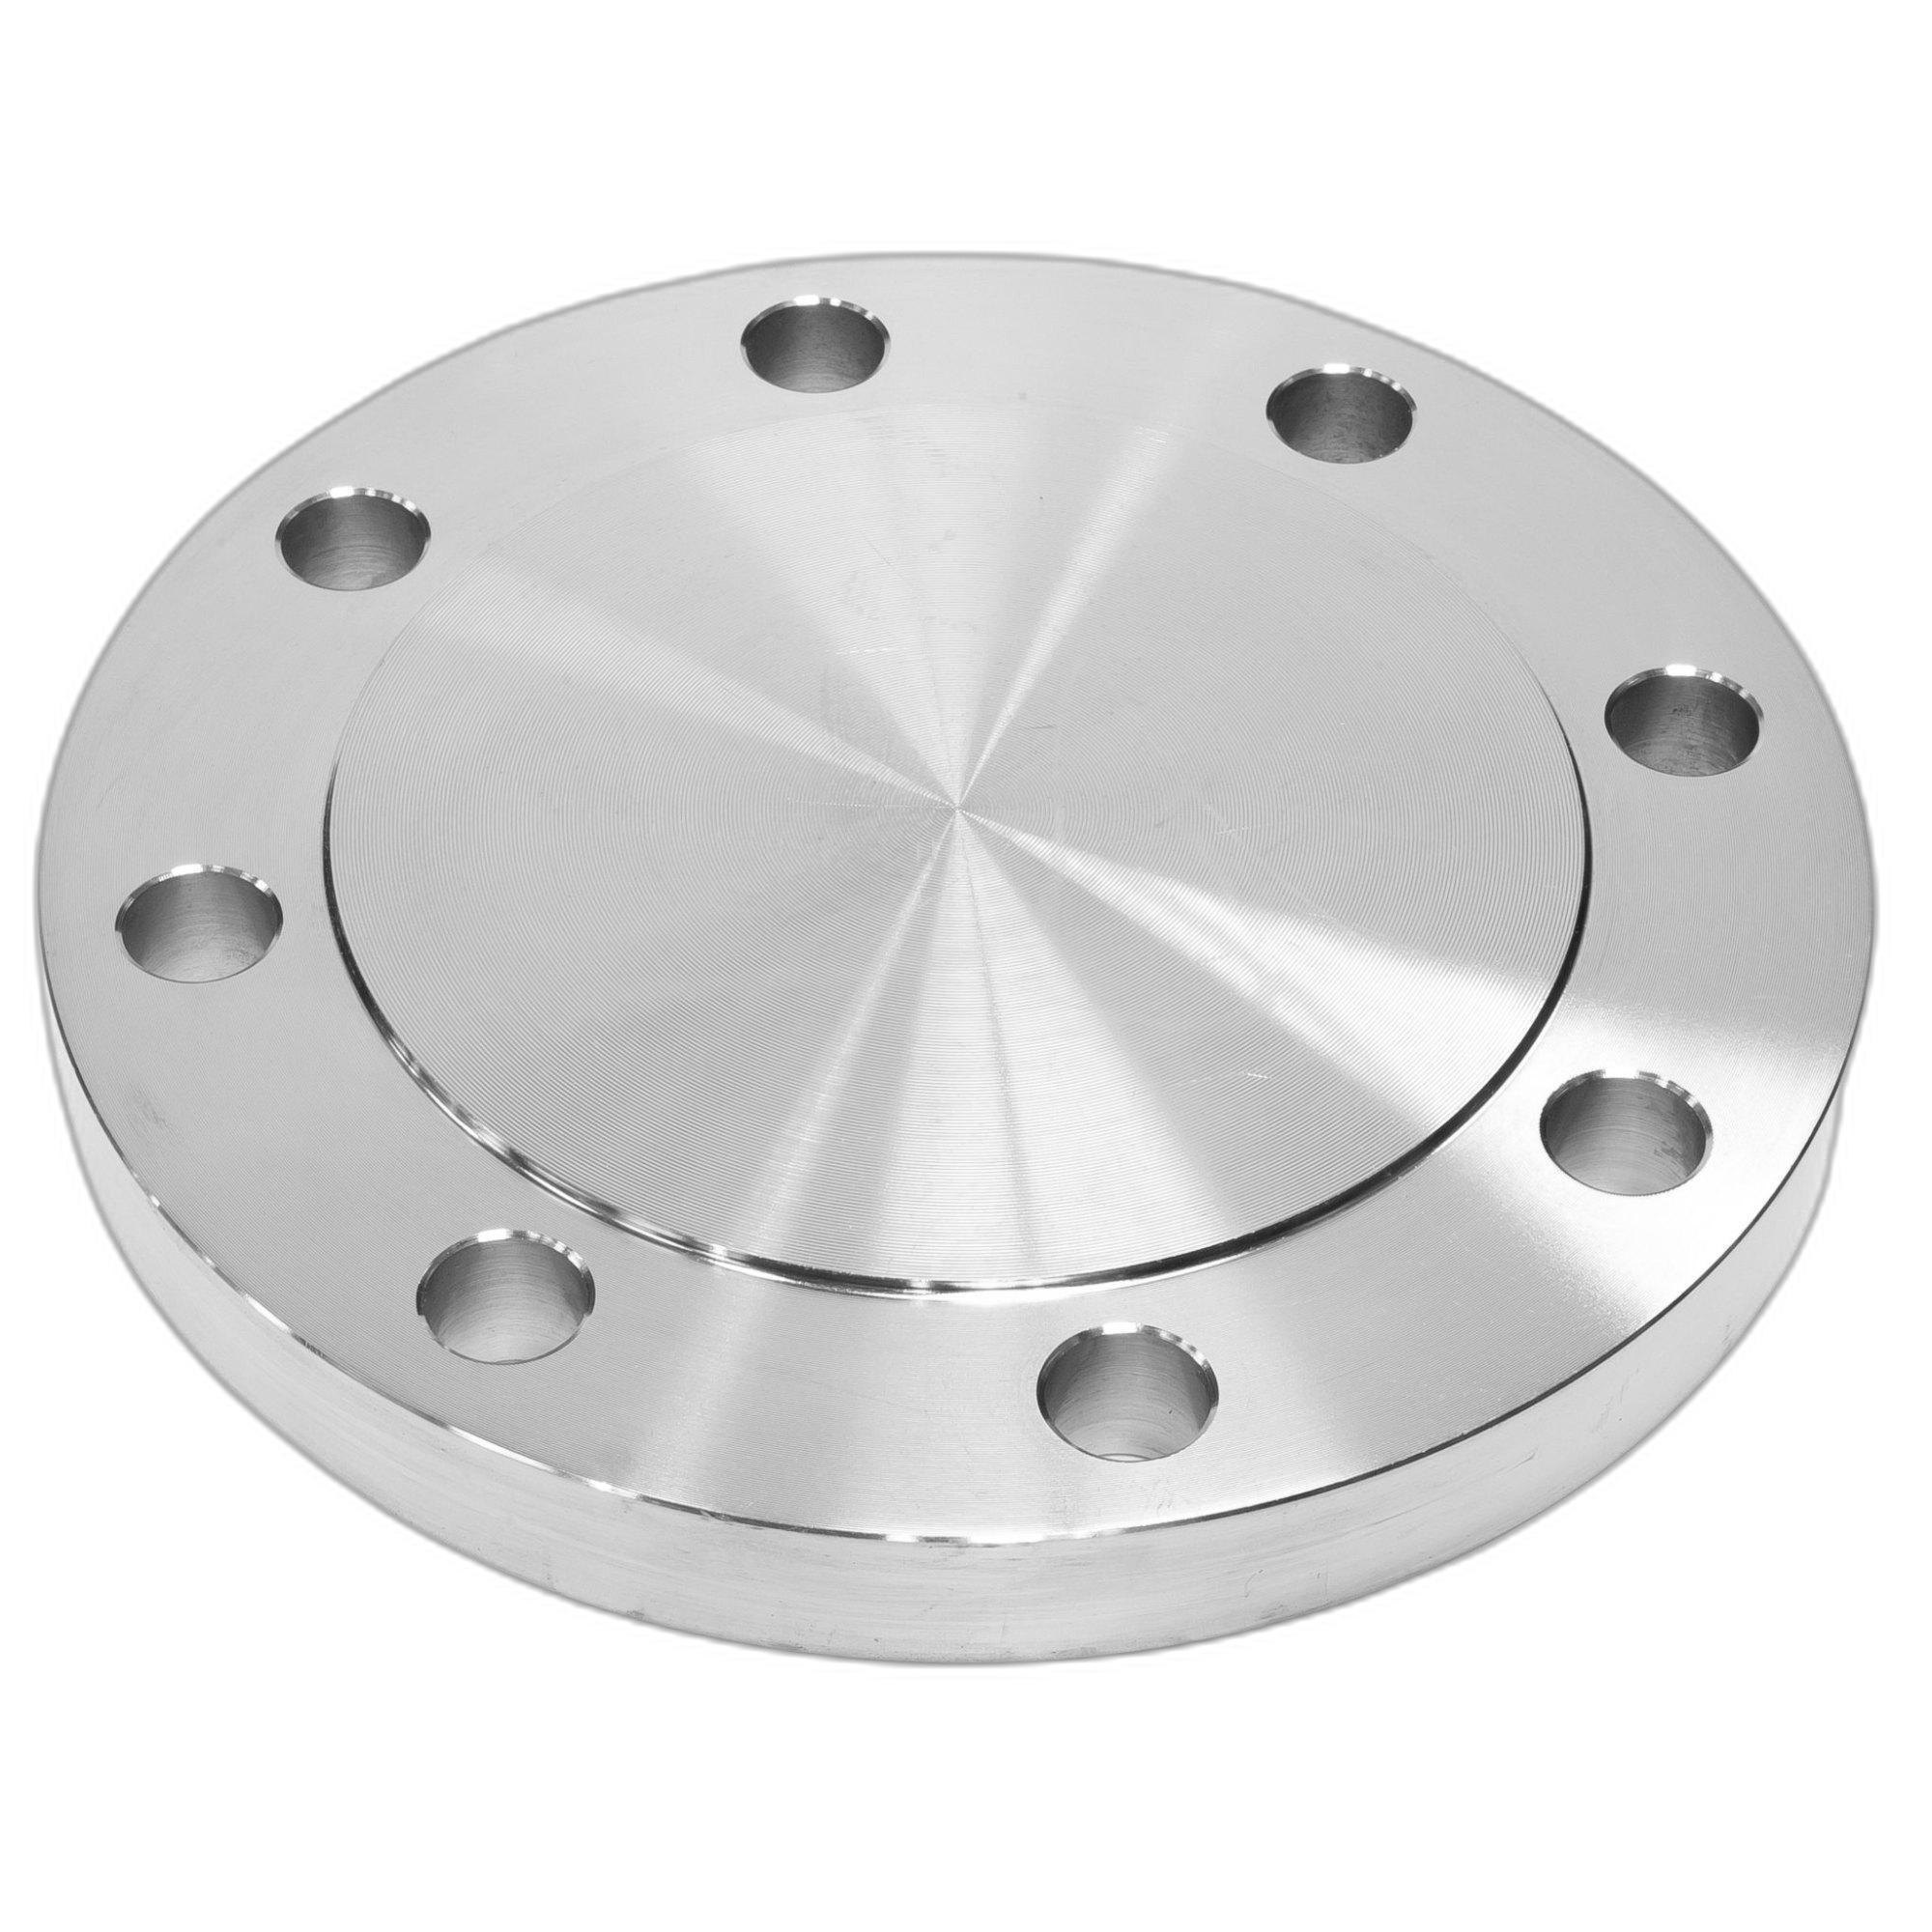
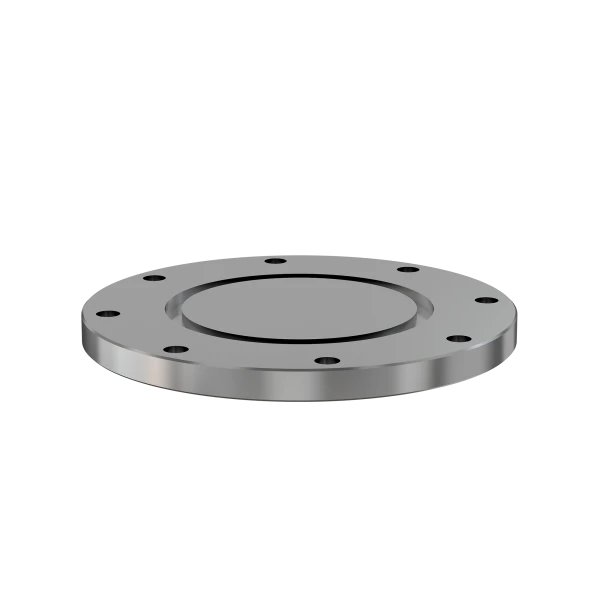
- ASA Blind Flange (BL): A solid forged disc with no center bore used to permanently seal specialized inspection openings or terminate a pipeline run under full hydrodynamic loads.
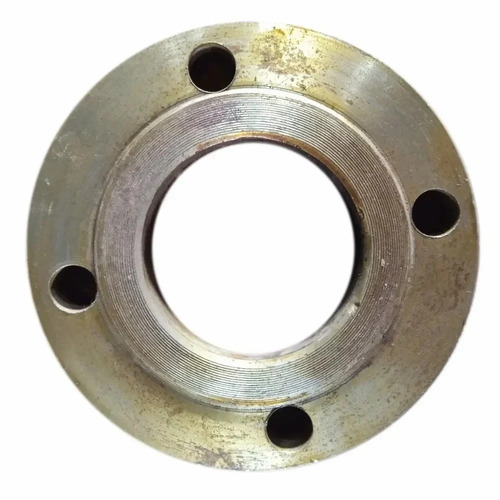
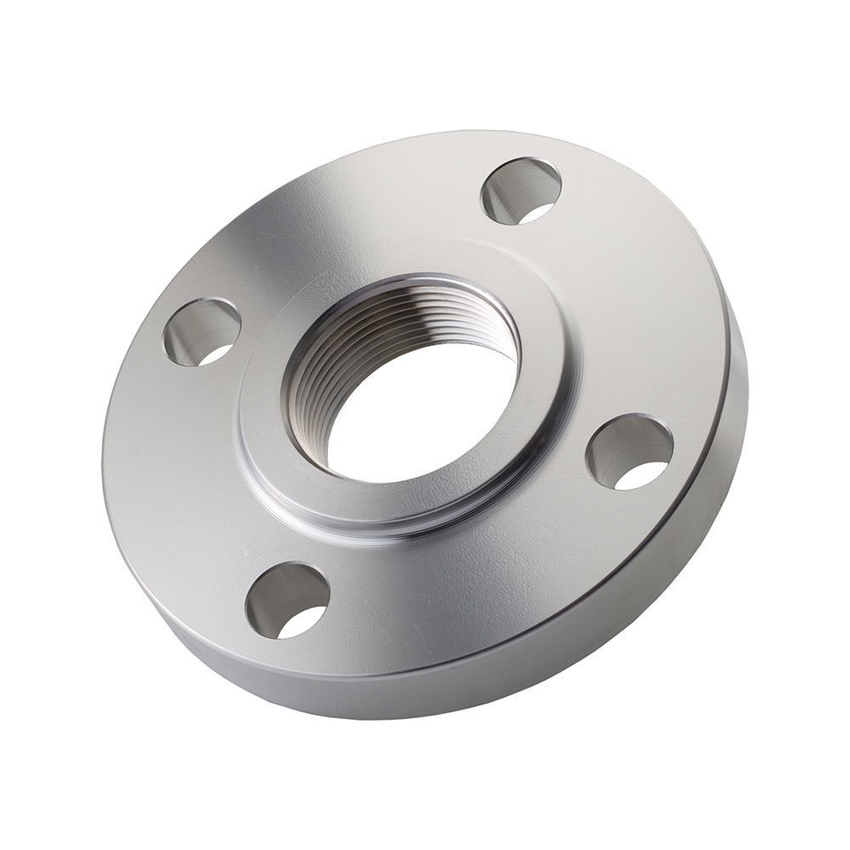
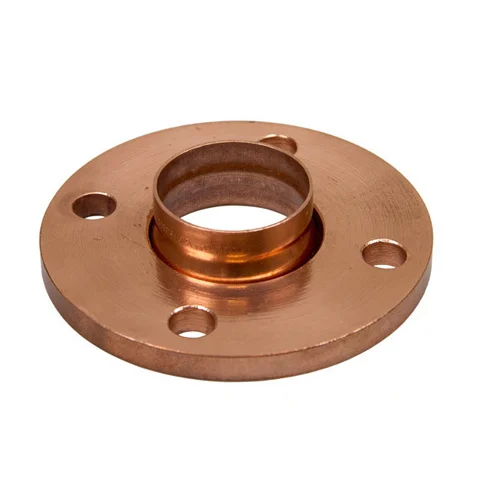
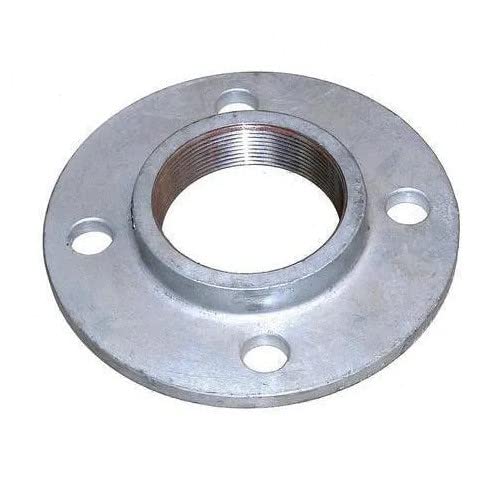
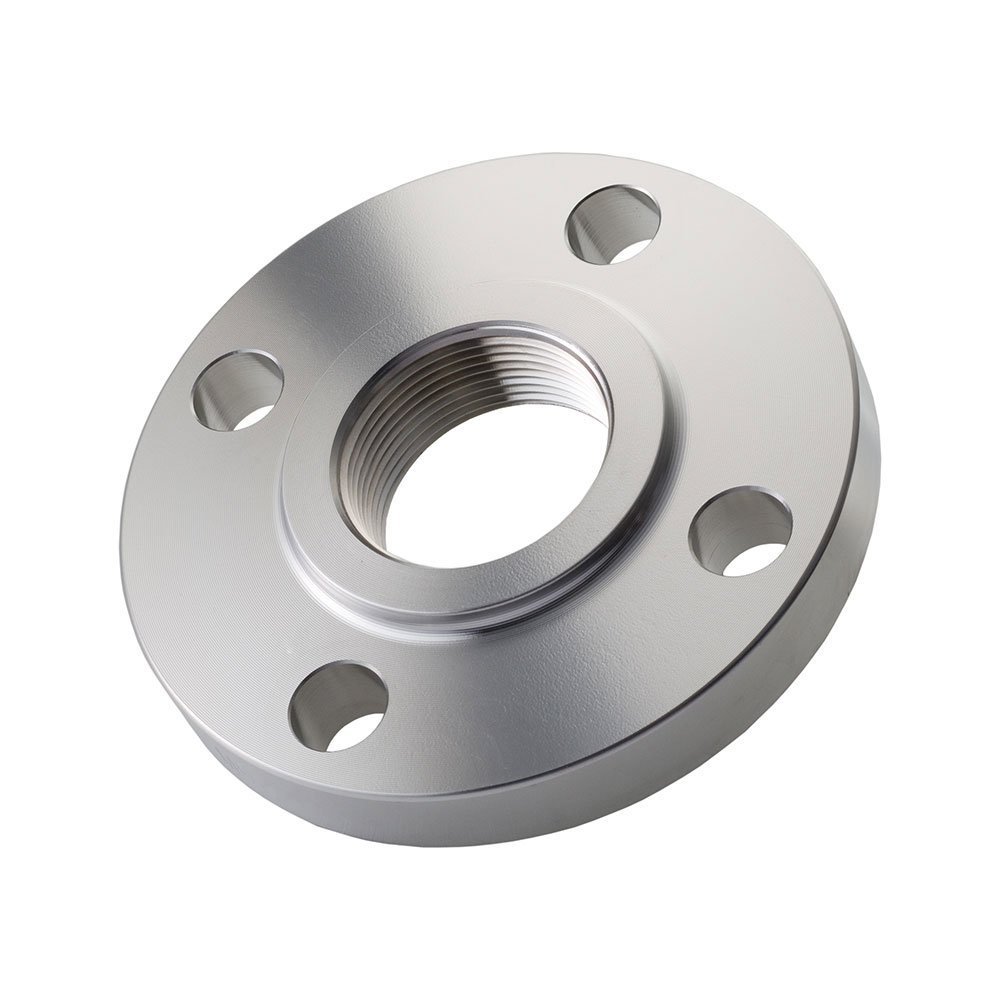
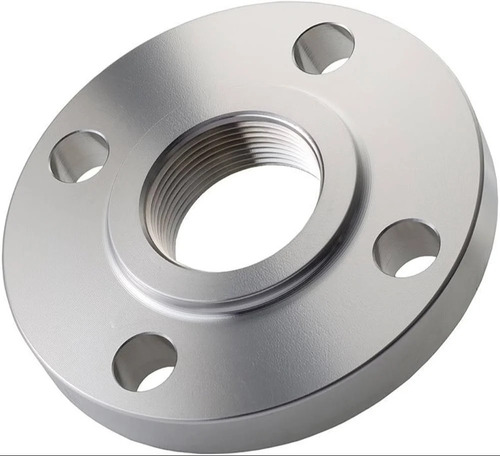
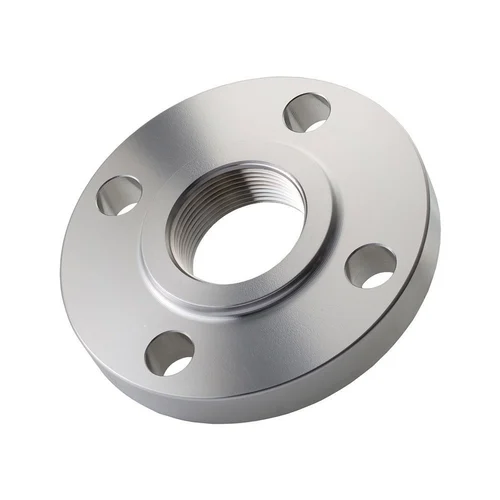
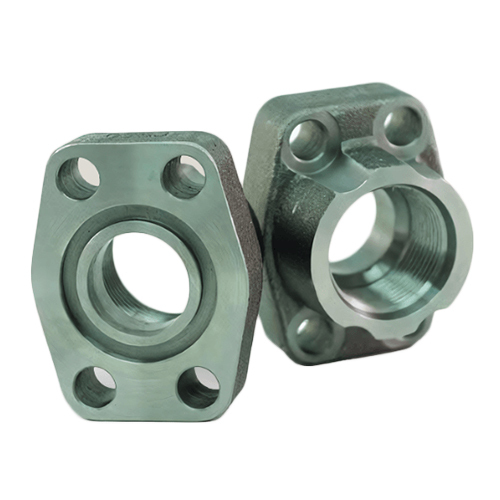
- ASA Threaded / Socket Weld: Engineered for small-bore piping networks where internal spaces limit welding options or where field welding is restricted.
Dimensional and Material Specifications
Our production engineering strictly follows historical dimensional codes to ensure hassle-free integration with legacy industrial machinery and existing piping infrastructure.
| Parameter |
Specification Details |
| Design Standards |
ASA B16.5 (Historical American Standard), ANSI B16.5, ASME B16.5, AWWA Class Matching Patterns |
| Material Carbon & Low-Temp |
ASTM A105, ASTM A350 LF2 Class 1/2, IS 2062 Grade A/B, A36 Structural Carbon |
| Material Stainless & Alloy |
ASTM A182 F304/304L, F316/316L, F11, F22, Duplex F51/F60, Super Duplex |
| Pressure Designations |
ASA 150 LBS / ASA 300 LBS / ASA 600 LBS (Direct cross-match to modern standards) |
| Facing Profiles |
Raised Face (RF), Flat Face (FF), Ring Type Joint (RTJ) |
| Size Range |
1/2” NB up to 24” NB (Custom large-diameter and heavy-wall structural dimensions available) |
| Testing Regimens |
100% PMI testing, Hydrostatic pressure validation, Face Flatness evaluation, LPT, CMM check |
Driving B2B Procurement via an Authorized Flanges Dealer in Mumbai
For global engineering, procurement, and construction (EPC) firms managing plant modifications or infrastructure restorations, coordinating specialized legacy joints is a precise task. Partnering with a dedicated distribution channel in Mumbai gives you a distinct operational edge.
We provide volume-based commercial discounts, comprehensive material traceability certifications (MTC EN 10204 3.1/3.2), and durable, sea-worthy packaging designed to prevent edge dents, thread cross-threading, or seating face scratches during transport. Additionally, our sales engineers provide direct technical support to procurement teams, verifying legacy bolt-circle diameters, matching schedule specs, and wall-thickness compatibility to match project parameters perfectly.
ASA Flanges Exporter in Mumbai
Fulfilling Global Contracts as a Top Flanges Exporter from Mumbai
Our focus on precision machining and zero-defect forging has earned strong international trust. Operating from the export hub of Mumbai, we regularly ship high-reliability ASA flanges to chemical chemical plants in the Middle East, structural piping installations in Europe, and water distribution networks across Southeast Asia.
Every export order passes through a strict final quality checkpoint, including full dimensional analysis, 100% PMI validation, and face flatness checks. We package shipments in heavy-duty, export-grade wooden cases equipped with moisture-resistant barriers and tailored face protectors. This ensures your components arrive at the project site ready for immediate installation.
Technical Specifications Summary
| ASA Flanges – Technical Specifications |
Details |
| Size Range |
1/2" to 24" (DN 15 to DN 600) / Custom dimensions on demand |
| Pressure Designation |
ASA 150 LBS, ASA 300 LBS, ASA 600 LBS |
| Type Configurations |
Weld Neck (WNRF), Slip-On (SORF), Socket Weld (SWRF), Blind (BLRF), Threaded Hubs |
| Face Design |
Raised Face (Serrated RF), Flat Face (FF), Ring Type Joint (RTJ Groove) |
| Manufacturing Process |
100% Hot Forged / Heat Treated & Precision CNC Machined Finished |
| Testing Protocols |
Hydrostatic, PMI, Hardness, CMM Dimensional Parity check, Liquid Penetrant |
| Certification Scope |
EN 10204 3.1 / 3.2 Mill Test Certificate, Material Grade Stamping Code Traceable |